Send Your Inquiry

Tell us about your application and the tools you need.

* Required fields

Skip to content
Spindle and workpiece in a machining enclosure

Corner Rounding End Mills

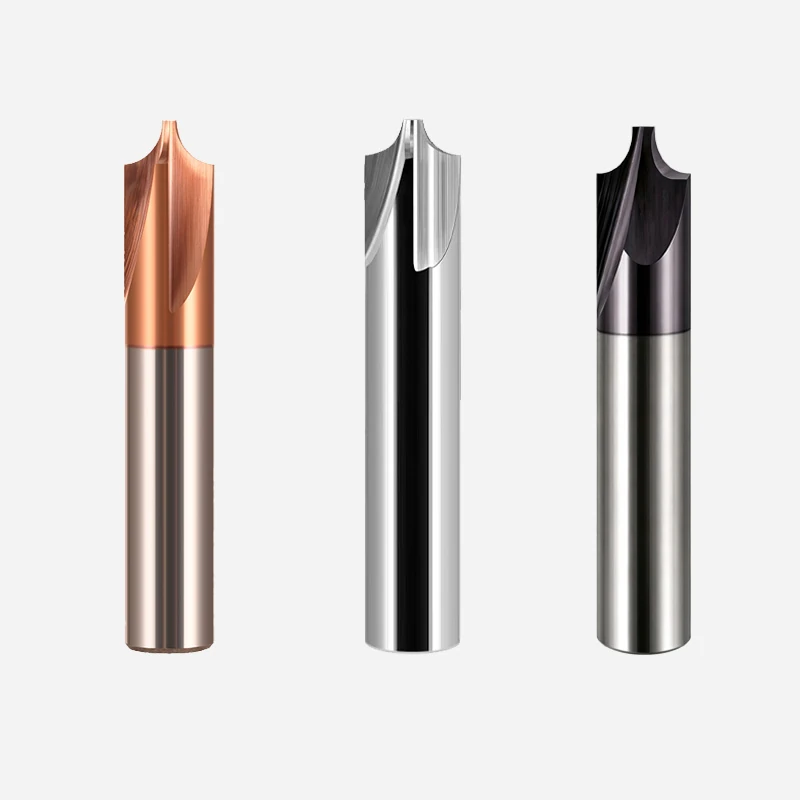
Corner rounding end mills form a radius on an external workpiece edge. MSU’s four-flute IRR carbide tools cover rounding radii from R0.5 to R8 mm.

Match the required edge radius first, then check pilot clearance, body diameter and access around the adjacent faces.

Send an IRR model and quantity, or an edge drawing showing the radius and clearance.

Find a Corner Rounding Tool

Corner Rounding Tools for External Edges

Use the IRR profile when the workpiece edge needs a rounded form.

Corner rounding end mills
IRR 4-Flute Corner Rounding Cutter Solid carbide · External-edge rounding
StartR0.5

R0.5–R8 mm

EndR8
Construction
Solid carbide
Flute count
4
Application
External-edge rounding
Selection basis
Drawing, clearance and setup

The edge profile and adjacent faces determine whether the cutter can reach the required radius.

Compare the radius, pilot and body dimensions against the edge.

Check Edge-Rounding Dimensions

Match the Edge Radius and Clearance

The radius defines the rounded form; the surrounding tool dimensions determine whether that form can reach the edge.

IRR radius and clearance dimensions.
DimensionMatch to the partWhy it matters
Rounding radius RFinished edge radius and toleranceDefines the required rounded profile
Pilot diameter d1Space beside the edgeChecks access around adjacent surfaces
Body diameter d2Clearance around the cutterThe body must not interfere with nearby walls or fixtures
Working reachDistance to the edge after clampingChecks access from the mounted holder
Shank and overall lengthHolder size and projectionCompletes the tool-to-machine fit

Check pilot clearance and body clearance on the approach and exit as well as during the cut.

Check how the cutter approaches the edge and clears nearby features.

Check Tool Approach

Selected IRR Model Dimensions

Selected IRR sizes in millimeters; each row is one defined combination.

Selected IRR sizes in millimeters; each row is one defined combination.
ModelRadius RPilot d1Body d2L1Shank Dh6Overall L
IRR-R0.50.51.52.75450
IRR-R111.53.75450
IRR-R221.55.75650
IRR-R331.57.710860
IRR-R44210.2151275
IRR-R8.08420.2202075

Use the drawing for the L1 reference and full profile. A larger rounding radius also changes the body and, for some sizes, the pilot and shank.

Check the model drawing for radius and clearance dimensions.

View IRR Dimensions

Define the Finished Edge

A section through the edge should show where the rounding starts and ends on the adjacent faces.

  • Radius callout: mark the required R, units and tolerance.
  • Adjacent faces: show steps or walls beside the rounded edge.
  • Edge extent: identify which edges require the same profile.
  • Workpiece: state the material grade and any finish requirement.
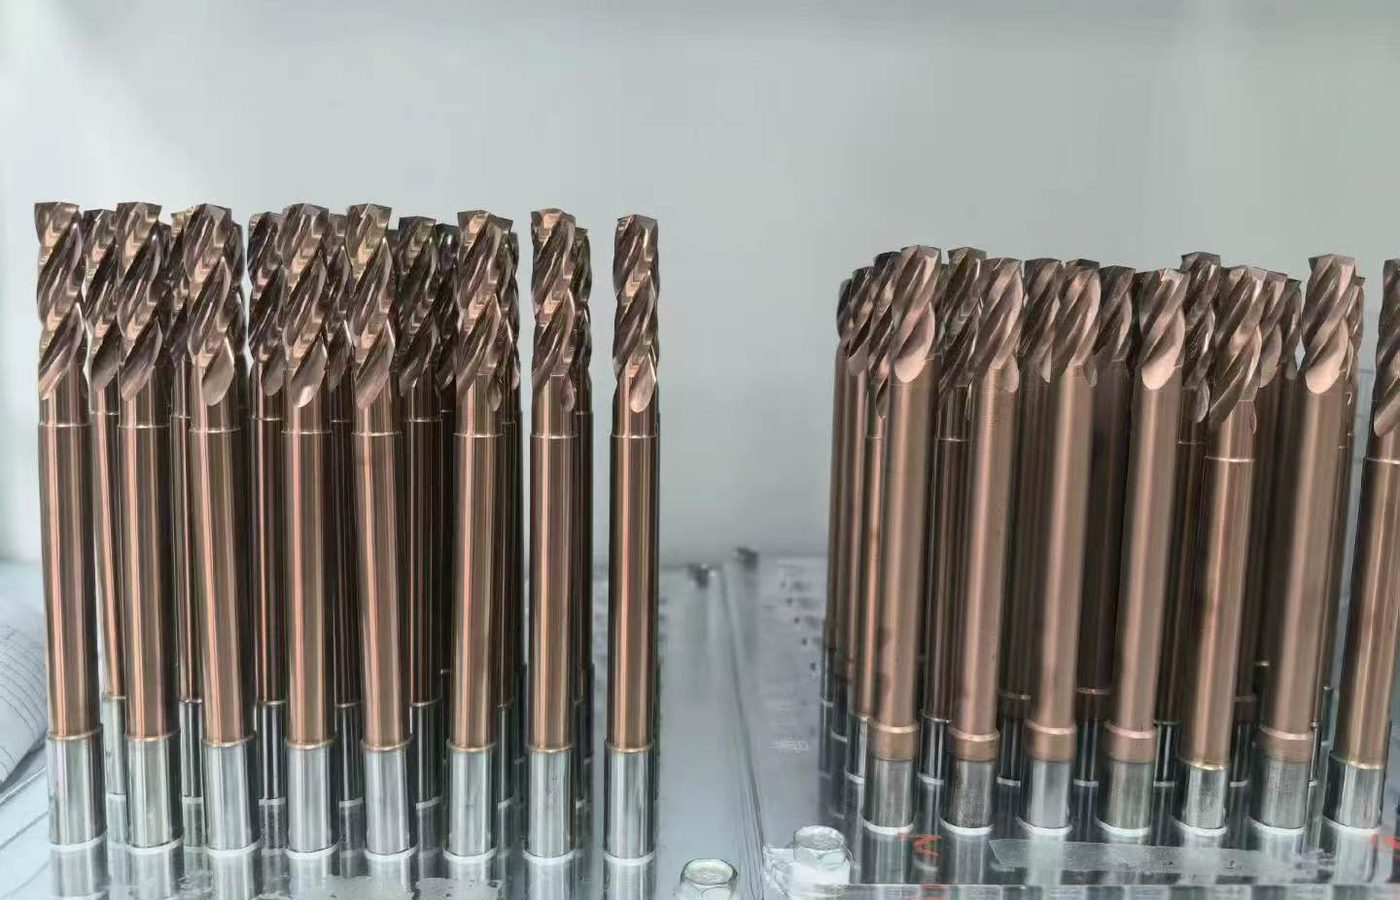
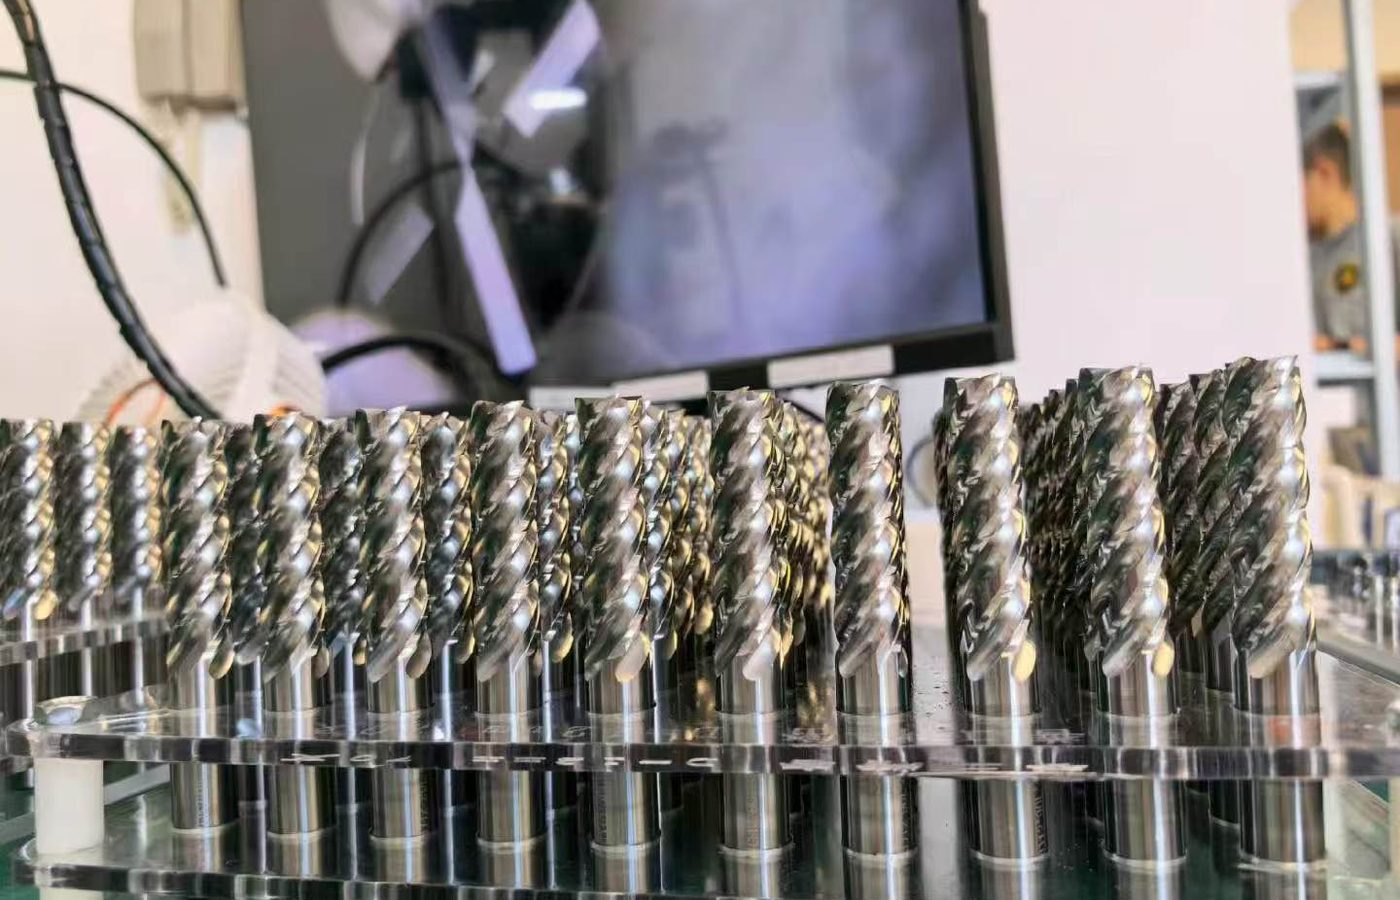
MSU carbide cutting tools

Tool selection

The End Mill Selection Guide covers general tool geometry. For a radius or access requirement outside these options, discuss Custom Cutting Tools.

Email the edge section if a wall or step limits access.

Discuss an Edge-Rounding Tool

Radius Profile and Inspection

Keep the tool profile requirement separate from the finished edge tolerance.

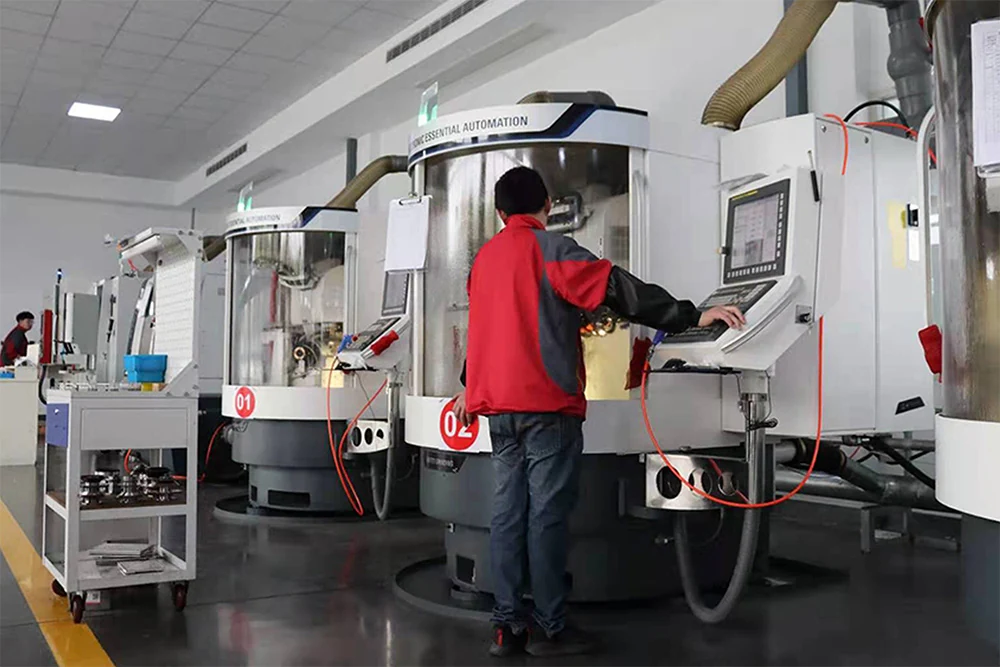
The MSU Factory has Walter HELITRONIC MICRO equipment; Quality Control facilities include a ZOLLER G3 measurement system.

The rounding radius defines the tool profile. Pilot and body diameters control access. Include these clearance dimensions on a custom tool drawing as well as the radius tolerance.

Operator using the control panel of a CNC tool grinder

Need a measurement report? State the tool dimensions to be reported with your enquiry.

Discuss Inspection Requirements

Request a Quote

For a repeat order, send the full model and quantity. For selection help, email the part detail and material to Maria.

MSU carbide cutting tools

MOQ

Normally 5–10 pieces; the quotation confirms the quantity for your selected tools.

Samples

Samples are charged. Sample freight is paid by the customer.

Lead time

Your quotation confirms production timing. Shipping time is stated separately.

Contact

Maria: maria@msutools.com · +86 13973369578 (phone or WhatsApp). Email drawings and photos.

Share the edge profile and required radius to confirm the cutter size.

Request a Quote

Corner Rounding Questions

No. The pilot and cutter body also need clearance beside the edge. The selected radius must be checked with its actual body and pilot dimensions.

No. Each IRR model has a defined combination. For example, IRR-R1 has a 1.5 mm pilot and 4 mm shank, while IRR-R4 has a 2 mm pilot and 12 mm shank.

The obstruction can restrict the pilot, body or holder approach. A section through both the edge and obstruction allows those clearances to be checked together.

Yes. Custom feasibility depends on the required radius, access and tool dimensions. Include the edge section, tolerances, material and quantity.