
Milling Inserts
Replace carbide milling inserts by matching the complete insert code to your cutter body and pocket. The range includes ONGU, ONMU, ODMT, APMT, WNMU, SNMU and round-insert families.
Once the fit is established, compare edge geometry and grade for the material, engagement and finish you need. Keep the cutter-body reference with the insert when ordering a replacement.
Send the full insert and cutter-body codes, with the quantity or machining issue to address.
Find a Milling InsertStart with Your Existing Cutter Body
The cutter pocket sets the required seating shape and dimensions. Select the matching insert family, then compare the complete designation and cutting-edge options.
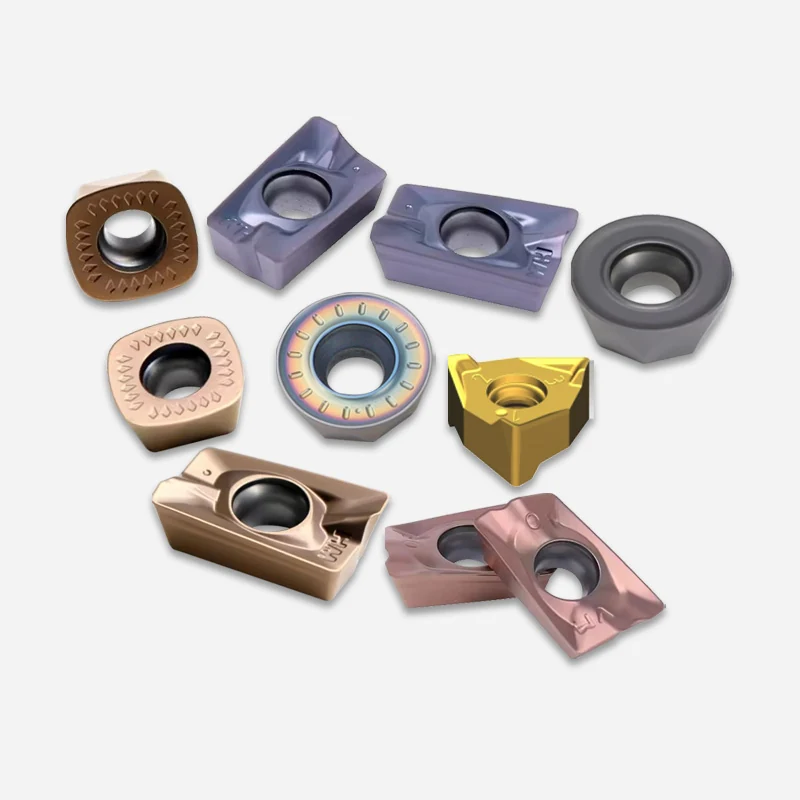
A matching family name still needs a matching size and seat.
Compare Milling Insert FitCheck Pocket Fit Before Changing the Edge
A similar-looking insert can have a different thickness, mounting hole or seating surface. Check those details before evaluating a change in geometry or grade.
| Selection factor | What to match | Effect on the choice |
|---|---|---|
| Cutter model | Full body reference and specified insert | Identifies the intended pocket and clamping system. |
| Insert shape | Seat outline and support surfaces | Establishes how the insert locates in the body. |
| Size and thickness | Drawing dimensions for the full code | Affects seating and cutting-edge position. |
| Mounting hole | Hole shape and screw or clamp specification | Must suit the body’s fastening arrangement. |
| Corner or round edge | Radius or round-insert diameter | Affects the feature and engagement at the cut. |
| Edge geometry | Suffix and edge preparation | Changes cutting behavior after fit is established. |
| Grade | Actual material grade and hardness | Guides the grade choice for wear and edge loading. |
| Engagement | Axial depth, radial width and entry conditions | Provides the cutting context for geometry and feed. |
| Assembly | Holder connection, projection and runout | Check the mounted cutter when finish or vibration changes. |
For uneven wear, compare the pockets and mounted assembly as well as the insert grade.
Check the Milling SetupDescribe the Cut and the Result to Improve
For a repeat order, use the current full insert reference. For a process change, identify the operation and what happens at the cutting edge.
- OperationState face milling, shoulder milling, profiling or the actual feature being cut.
- Cutter and insertRecord body model, diameter, number of pockets and full insert designation.
- WorkpieceInclude material grade, hardness, scale and interrupted surfaces.
- EngagementState axial depth and radial width, plus how the cutter enters the material.
- Current cutting dataRecord speed, feed per tooth and coolant method.
- ResultDescribe finish marks, vibration, chipping or uneven wear by pocket position.
Include the cutter-body code and photos of the used edges when discussing a milling problem.
Discuss a Milling InsertCompare Milling Families and Size Examples
These examples identify individual sizes within the families. Use the complete designation with the grade; the dimensions below are in millimeters.
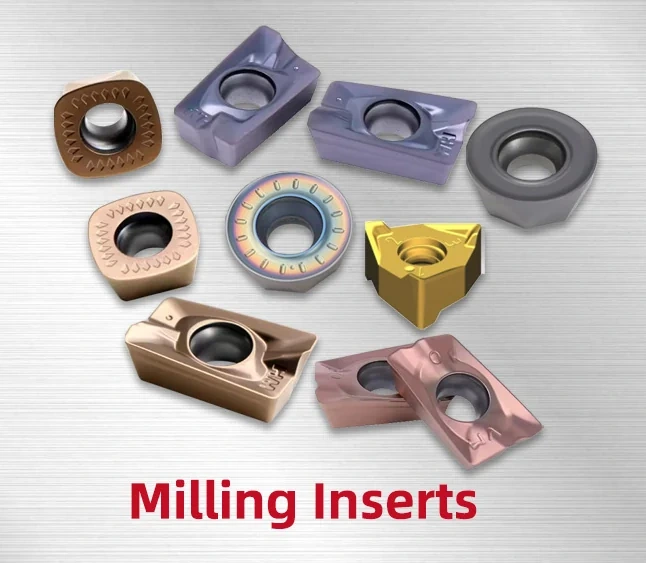
ONGU050403-CR · L 5.26, W 12.7, S 4.76, d 4.4, Re 0.3.
ONMU060408-CR · L 6.58, W 15.875, S 4.9, d 4.35, Re 0.8.
ODMT050408-CR · L 5.26, W 12.7, S 4.76, d 4.4, Re 0.8.
APMT1135PDER-CM · L 11.25, W 6.26, S 3.5, d 2.8, Re 0.8.
WNMU060408R-YM · L 6.41, W 10.15, S 4.36, d 4.2, Re 0.8.
SNMU1206ANN-Y · L 12, W 12.7, S 5.5, d 5.95, Re 0.8.
RPMT1003MO-CM · IC 10, S 3.18, d 4.6.
RPGT1204MO-MR · IC 12, S 4.76, d 4.45.
RPMW1003MO · IC 10, S 3.18, d 4.6.
RPGW1003MOEN · IC 10, S 3.18, d 4.6.
RDMW10T3MOTN · IC 10, S 3.97, d 4.4.
Read the milling-insert drawing
- L and W: dimensions shown for the selected shape
- IC: inscribed circle or round-insert diameter
- S: insert thickness
- d: mounting-hole dimension
- Re: corner radius where specified
- Complete suffix and selected grade
Find the drawings in Downloads. The 10 mm round-insert examples illustrate why matching diameter alone is insufficient: thickness and hole dimensions can differ.
Use the dimension drawing and full designation to identify the insert you need.
View Insert DimensionsCheck Seating and the Milled Result
Specify the insert dimensions to check against the cutter. For a trial, define the finished surface and dimensional limits on the component drawing.
See MSU Factory and Quality Control for equipment and tool-measurement information.
If finish or size changes after indexing, record the pocket positions, seating condition and mounted measurements alongside the used-edge photos.
State any insert measurements and inspection records required before ordering.
View Inspection InformationOrder a Replacement or Discuss a Drawing
For a repeat order, use the full insert reference and grade. For a new application, email the drawing and identify the machining problem or feature that needs attention.
Repeat orders
Send the complete insert designation, geometry suffix, grade and quantity, or your previous order number.
New applications
Include the cutter-body model, material, engagement and current cutting conditions. Email drawings to Maria using the address below.
MOQ and samples
MOQ is normally 5–10 pieces, confirmed for the selected product. Samples and sample freight are charged.
Delivery and payment
Availability, production and shipping timing are confirmed in the quotation. T/T deposit and balance terms are stated with the order.
Purchasing information
Ordering and Delivery covers purchasing terms; Downloads provides insert drawings.
Contact
Email Maria at maria@msutools.com or call/WhatsApp +86 13973369578.
Review the purchasing terms when confirming the selected insert, quantity and delivery.
View Ordering and DeliveryMilling Inserts Questions
Answers to common fit, selection and replacement questions.
Match the complete insert designation and dimensions to the cutter’s specified insert. The family name alone leaves size, seating and fastening details unresolved.
Compare thickness, mounting hole, seat geometry and complete suffix as well as diameter. The 10 mm examples shown include different thickness and hole dimensions.
Specify the inserts and quantities required. The cutter-body reference is used to match the replacement; the quotation lists the supplied items.
First establish that the insert geometry and mounting fit are unchanged. Then choose the grade for the material and engagement, and review cutting conditions for the proposed insert.
Record the affected pocket, seating condition and mounted runout alongside the insert reference and cutting data. Compare the other pockets before attributing the difference to grade alone.
Include the cutter model, insert reference, material, axial and radial engagement, feed per tooth and mounted setup. Show the surface marks and condition of the used edges.
Send the full insert designation, grade and quantity, or the previous order number. Add the cutter-body code when cross-referencing a replacement.