Micro Drills
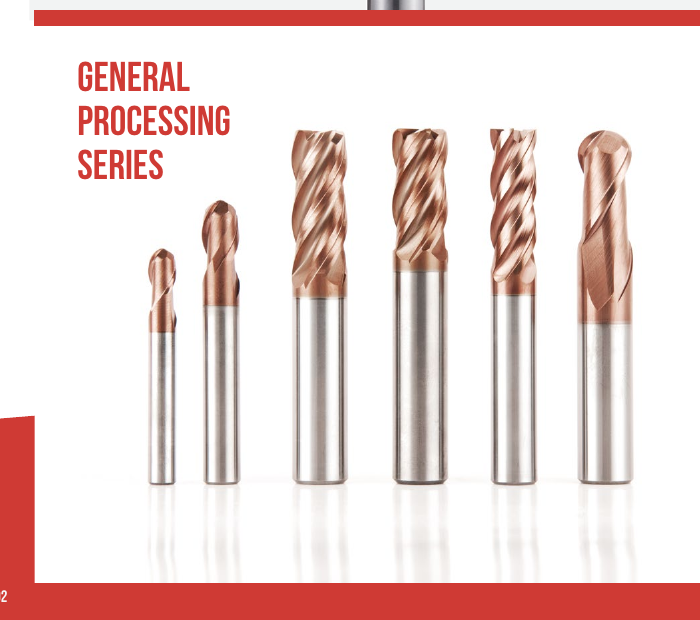
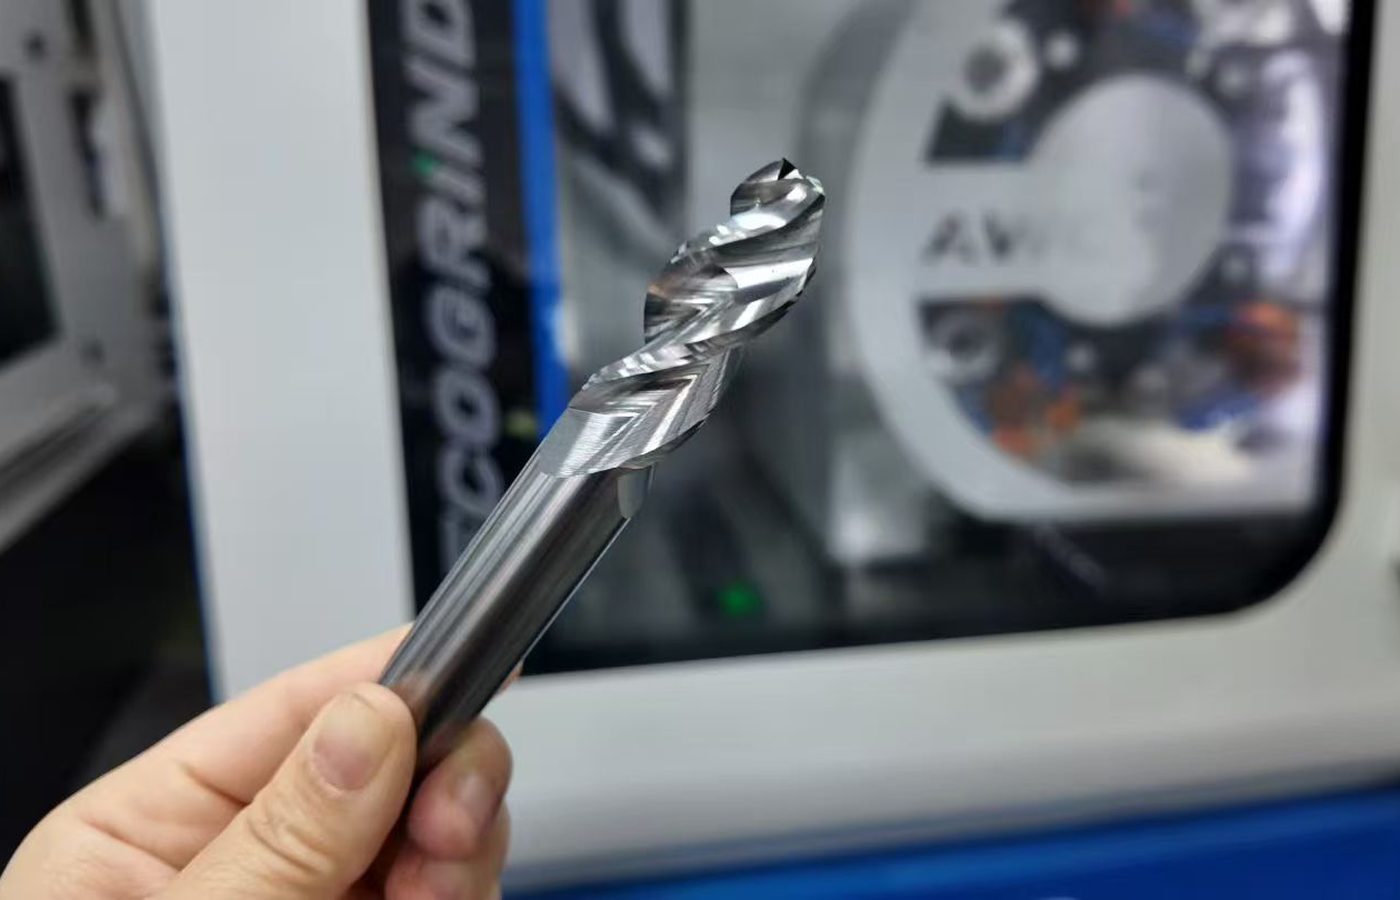
For small holes, compare diameter, point angle and regular or extra-long flute options. Check the working length at the exact diameter you need.

Find a drill for a new hole or a reamer to finish an existing one. MSU offers solid carbide micro drills, 3D–8D drills, 10D–30D deep-hole drills, replaceable-head systems and solid carbide reamers.
Start with the hole diameter, depth and final tolerance. Then compare the tool’s reach, coolant requirements and fit with your machine.
Send a hole drawing for a new job, or the tool reference and quantity for a repeat order.
Find a Holemaking ToolDrilling creates the hole; reaming removes a small allowance from an existing hole to finish its size and surface. A replaceable-head system lets you select the cutting components and drill body together.
Replacing an SPMG or WCMX cutting insert? See Shallow Hole Drilling Inserts. For machine-side clamping, compare Toolholders; for other machining operations, see Cutting Tool Products.
For small holes, compare diameter, point angle and regular or extra-long flute options. Check the working length at the exact diameter you need.
For 3D, 5D and 8D drilling, compare external- and internal-coolant models with the coolant supply available on your machine.
For 10D–30D drilling, check usable depth, entry guidance, coolant delivery and the space needed for the complete assembly.
Replace a cutting head or specify a complete drill assembly. Head, body and connection references must match.
Finish a prepared hole to its specified size and surface. Choose around the pre-hole condition, remaining allowance and coolant supply.
Match the operation first, then compare the dimensions and setup.
Compare Holemaking OptionsThe same nominal diameter can be offered in different tool constructions. The existing process and required hole depth help narrow the choice.
A depth ratio relates hole depth to diameter. The selected drill still needs sufficient working length, point clearance and room for chips to leave the hole.
| Product type | Use it for | Selection priority |
|---|---|---|
| Micro Drills | Small-diameter holes | Diameter and flute length; spindle and holder runout |
| Solid Carbide Drills | One-piece drills in 3D, 5D and 8D lengths | Hole depth and external or internal coolant |
| Solid Carbide Deep Hole Drills | Long holes in the 10D–30D range | Entry guidance, working reach and coolant delivery |
| Replaceable Head Drills | A replaceable cutting head with a matched body | Component codes and assembled dimensions |
| Solid Carbide Reamers | Finishing a pre-machined hole | Pre-hole size, allowance and final inspection |
Consider the finished hole as well as the operation that comes before it.
Check the Hole RequirementsA through hole needs exit clearance. A blind hole needs enough depth for the cutting end as well as the required full-diameter section. Include these features when comparing tools.
For an existing machining problem, keep the tool reference and a measurement of the affected hole. Note whether the issue occurs at entry, along the bore or at breakthrough.
For stepped holes or dimensions outside the standard sizes, email the part drawing to discuss Custom Cutting Tools.
Email the hole drawing with the material and the feature that is difficult to machine.
Discuss a Holemaking JobUse Downloads for dimension drawings. Each tool type has its own length and diameter symbols, so use the drawing that belongs to the selected model.
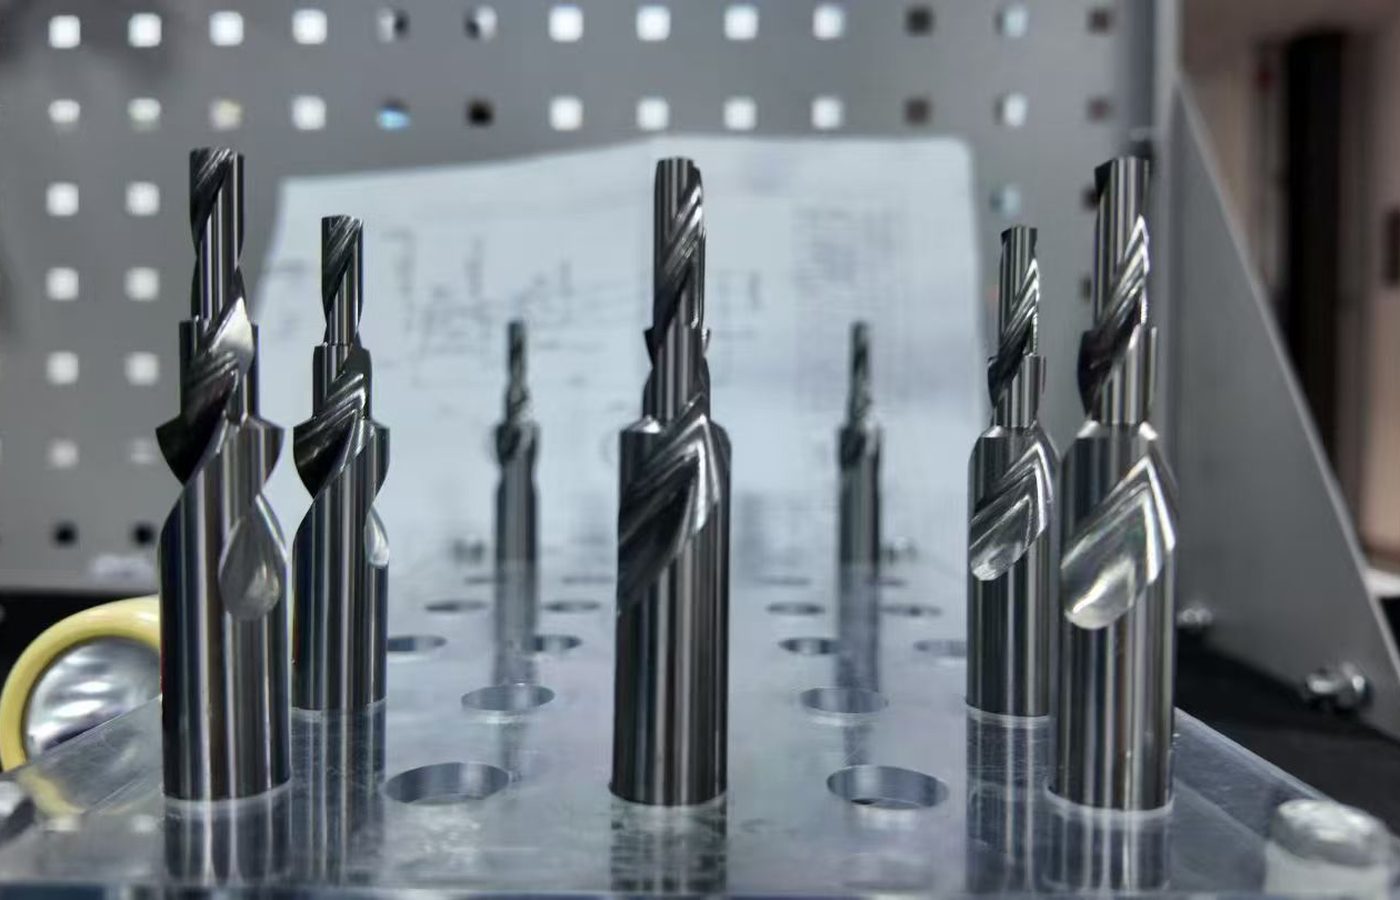
| Tool type | Available options | Dimension or fit to check |
|---|---|---|
| Micro Drills | 326, 326L, 426 and 426L | Cutting diameter, flute length and point angle |
| Solid Carbide Drills | MGP and MGPP: 3D/5D; MGPC: 3D/5D/8D | Flute length, shank and coolant construction |
| Solid Carbide Deep Hole Drills | 10D, 15D, 20D, 25D and 30D | Working reach and total assembly length |
| Replaceable Head Drills | Mono Tip and Multi Tip | Head, body, interface and component list |
| Solid Carbide Reamers | REA-H7 and REAC-H7 | Cutting diameter, flute count and coolant |
Use the selected model’s drawing to check dimensions before ordering.
View Holemaking DimensionsSpecify how diameter, depth and any controlled surface or position will be measured. Tool inspection and finished-hole inspection answer different questions.
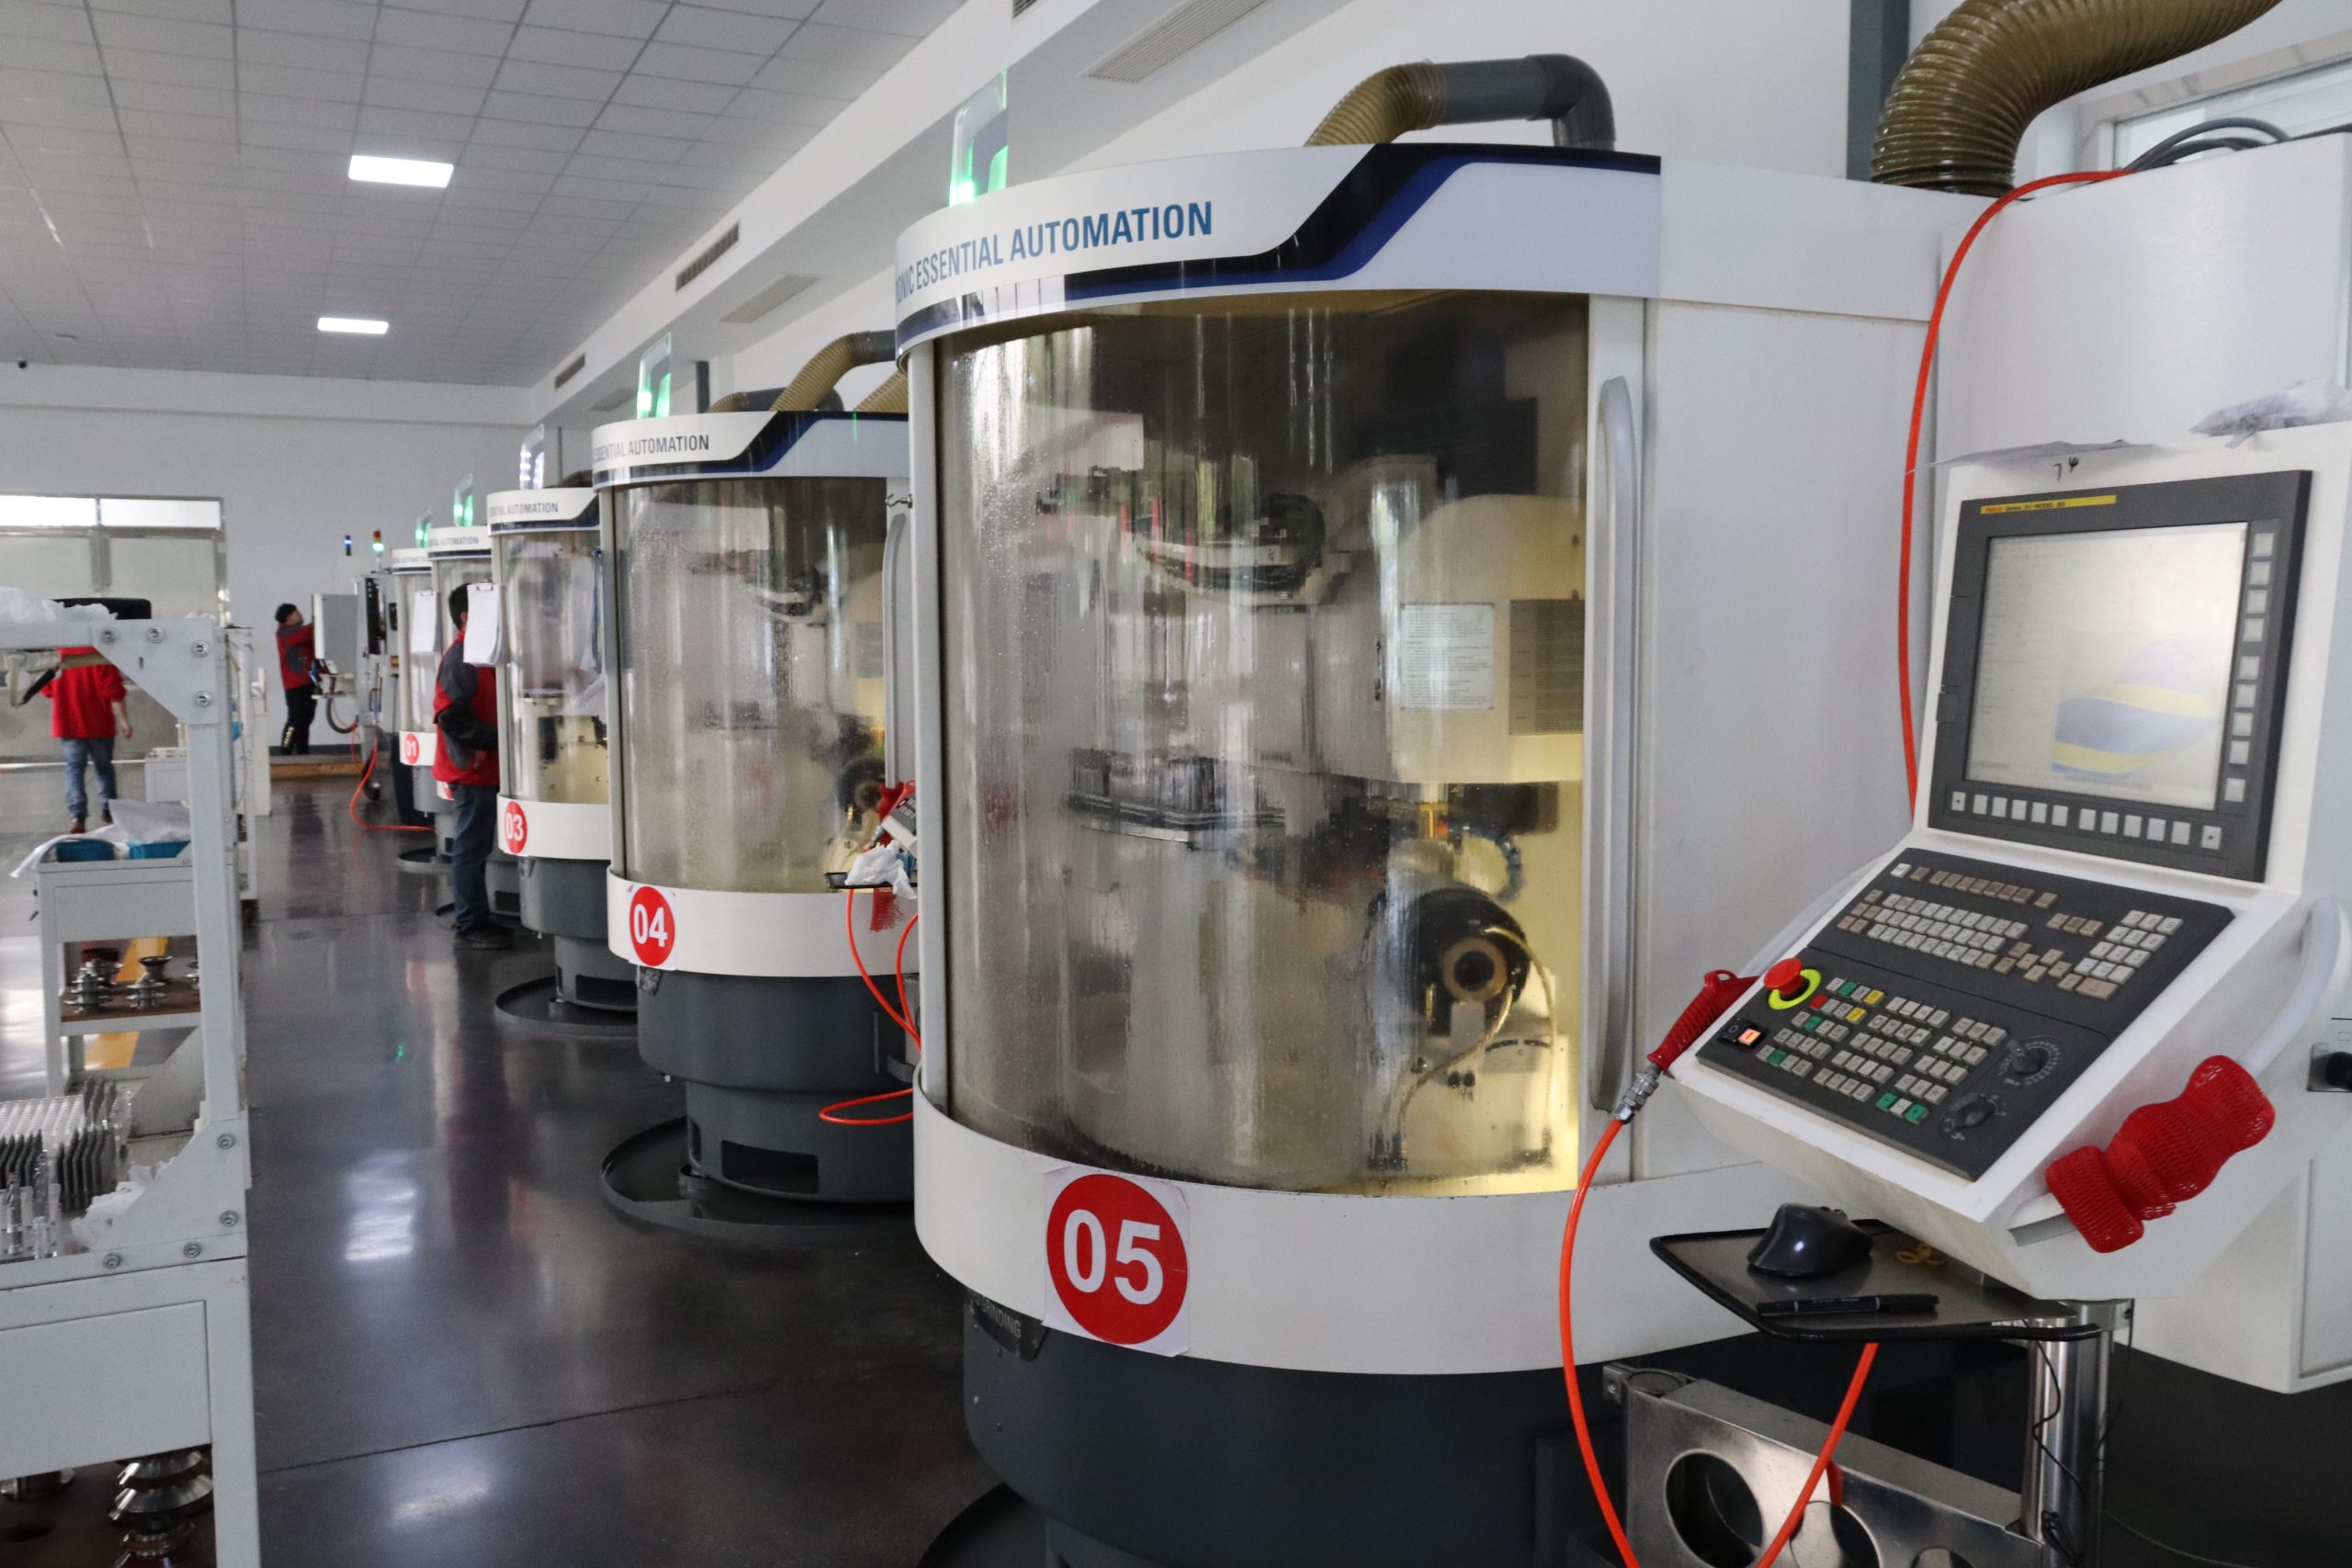
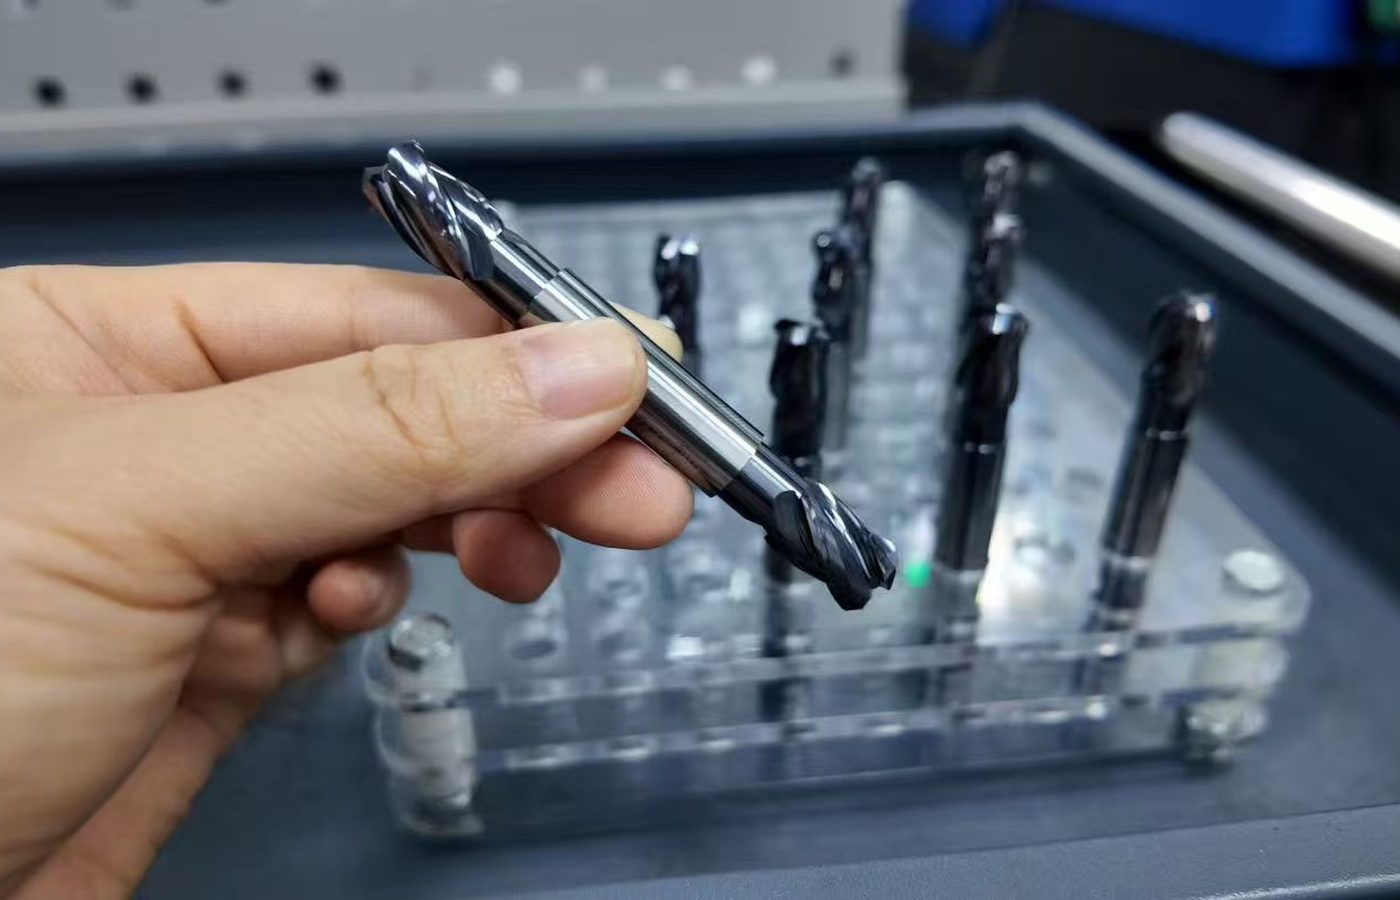
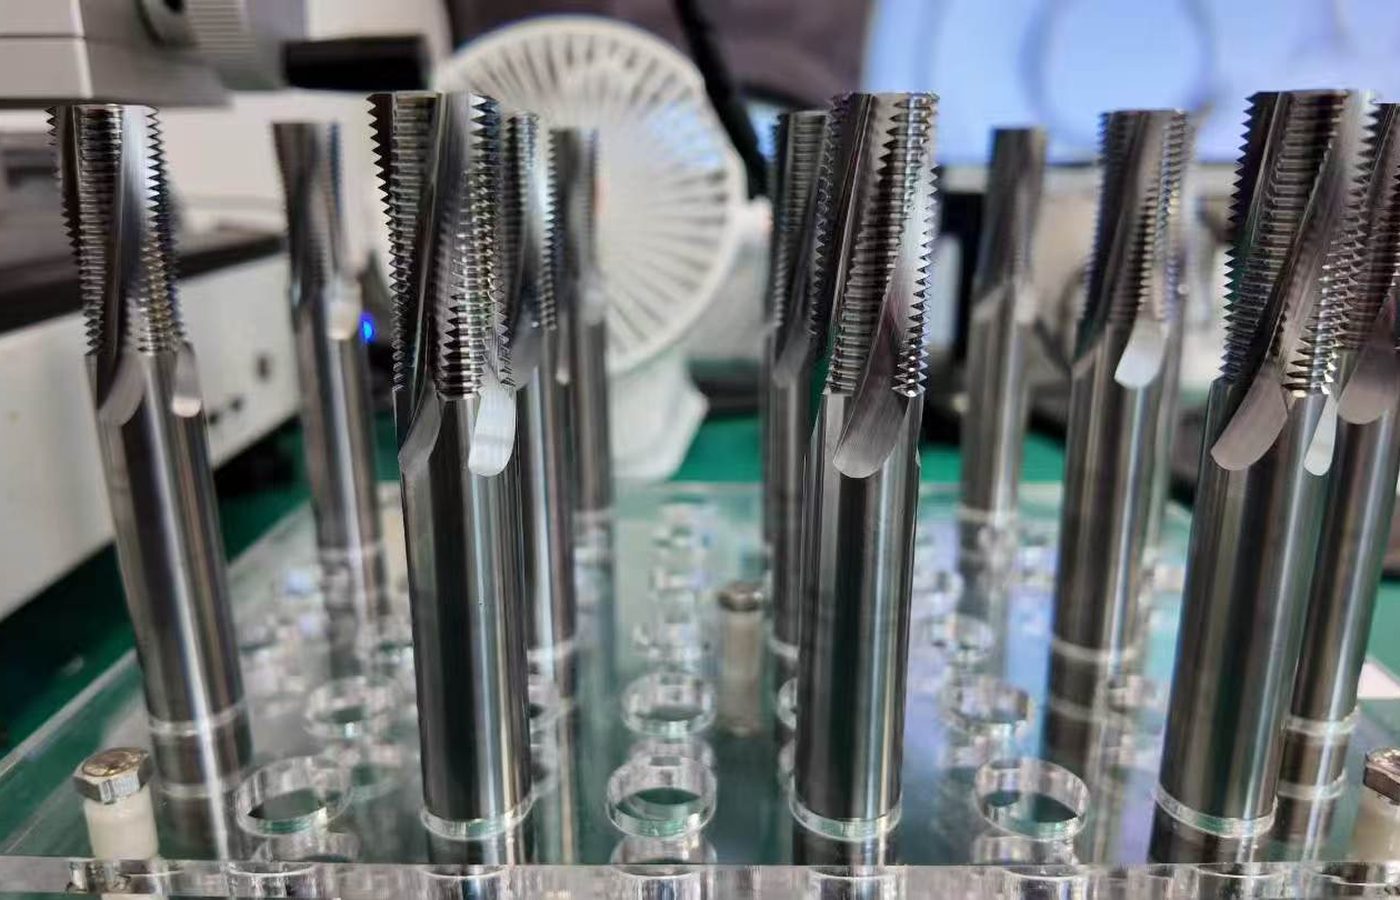
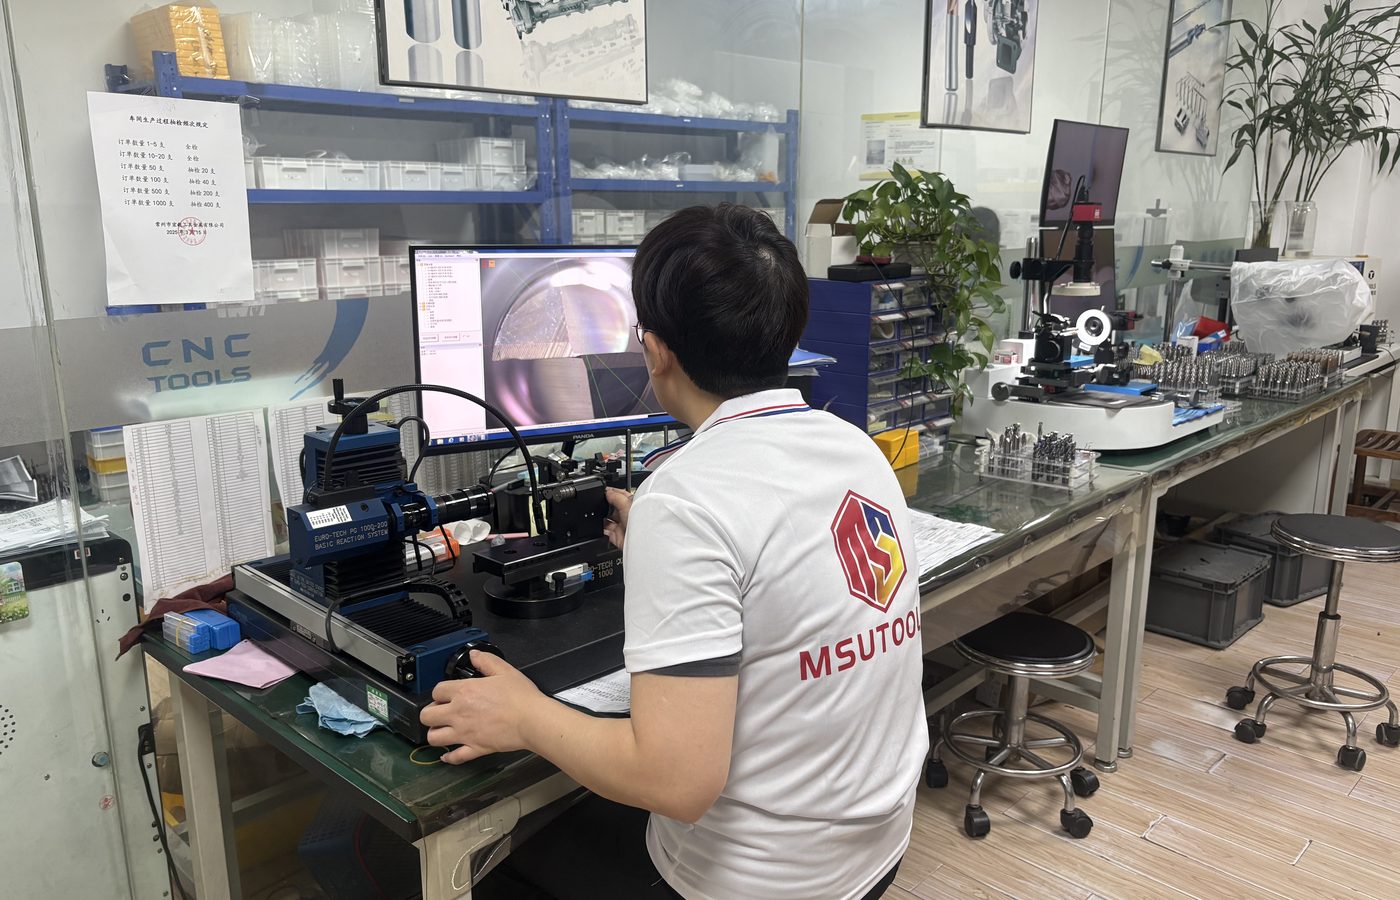
See MSU Factory and Quality Control for equipment and tool-measurement information.
For a trial, keep the tool reference and setup with the hole measurements so a dimensional issue can be traced to the relevant operation.
Specify the tool measurements and records required before placing the order.
View Tool Inspection InformationThe quotation will identify the selected tools or components, quantity, delivery terms and any agreed inspection records.
Use the full tool or component reference and quantity, or the previous order number. Mention any change to the application.
Email the hole drawing and material. Highlight the depth, tolerance, clearance or machining problem that needs attention.
MOQ is normally 5–10 pieces, confirmed for the selected product. Samples and sample freight are charged.
Production and shipping timing are confirmed in the quotation. T/T deposit and balance terms are stated with the order.
See Ordering and Delivery for purchasing terms and Downloads for dimension drawings.
Email Maria at maria@msutools.com or call/WhatsApp +86 13973369578.
Check the purchasing terms when confirming your tool reference, quantity and delivery.
View Ordering and DeliveryUse a drill to create the hole. Reaming is a finishing operation on a prepared hole with a controlled allowance. If the final size or finish needs a separate finishing cut, define that requirement before selecting the pre-hole drill.
The solid carbide drill range includes 3D, 5D and 8D options; deep-hole drills cover 10D through 30D. Compare the required hole depth with the actual tool dimensions and assembled reach.
It may reach the hole, but additional projection changes the setup. Use the shortest tool and mounted length that provide the required depth and clearance.
Use the full reference of the component and the body it fits. For SPMG or WCMX inserts, compare Shallow Hole Drilling Inserts. For a replaceable-head assembly, identify both the head and drill body.
Yes. Email the part drawing with the material, hole dimensions and machine constraints. The proposed geometry and inspection requirements can then be agreed.
Send the full tool reference or previous order number, quantity and any change to the application. For an assembly, state which components you need.
Production timing, availability and shipping are confirmed in the quotation for the selected tools, quantity and destination.