
Steel & Pre-Hardened Steel Milling
Choose an end mill for steel around the cut you need to make: a slot, shoulder, flat floor or curved surface. MSU offers GP, GPP and HPX carbide tools with square, ball-nose and corner-radius profiles.
These families cover material conditions below 55 HRC. For pre-hardened steel, use the measured hardness and steel grade together. For higher-hardness workpieces, compare Hardened Steel Milling.
Send a tool code and quantity, or describe the steel and feature you need to machine.
Find a Steel Milling ToolMatch the Steel and the Cut
The steel grade and heat-treatment condition narrow the tool choice. The feature then determines the end profile, cutting length and access you need.
- Flat floors and shoulders Choose a flat cutting end and check the required corner detail.
- Curved surfaces Match the ball radius to the contour and surrounding features.
- Corner radii Match the tool-end radius to the floor-to-wall detail on the drawing.
- Slots and open sides A full-width slot and a light side cut engage the tool differently; use cutting conditions for the intended operation.
- Deep features Check the cutting length and holder clearance separately. Overall tool length alone does not establish usable reach.
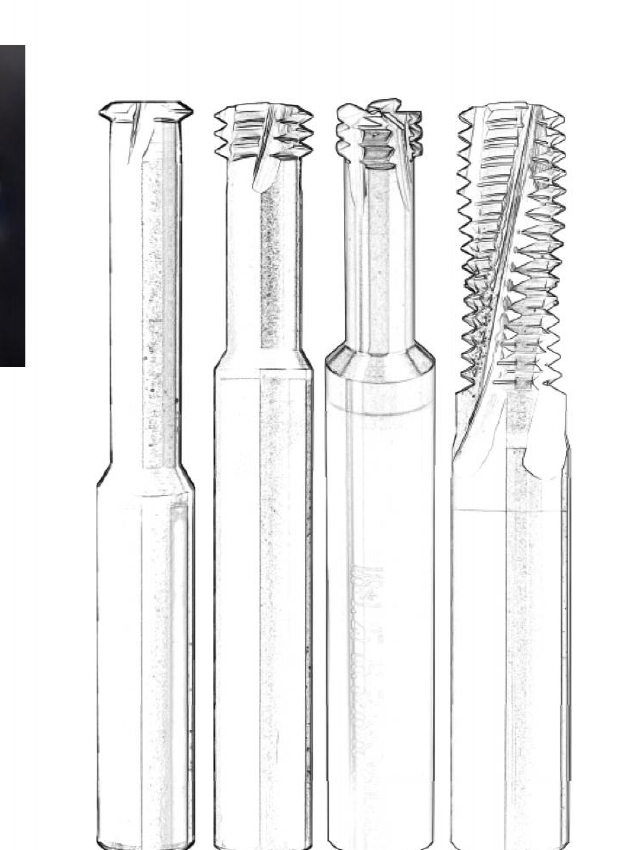
For a roughing pass, allow for the stock that must remain for finishing. For the final pass, identify the surface and tolerance that the toolpath must produce.
Compare the available profiles and diameter ranges for your feature.
Compare Steel Milling ToolsCompare GP, GPP and HPX Tools
The Carbide End Mills range includes the following families. Compare end profile and dimensions before selecting a full model; the series name alone does not rank the tools for your job.
| Series | Tool families | End profile | Diameter and hardness range | Feature |
|---|---|---|---|---|
| GP | GPE2, GPE4 | Square End Mills | 1-20 mm; below 55 HRC | Flat floors and shoulders |
| GP | GPB2, GPB4 | Ball Nose End Mills | 1-20 mm; below 55 HRC | Curved surfaces and contours |
| GP | GPR4 | Corner Radius End Mills | 1-20 mm; below 55 HRC | Floors with a specified corner radius |
| GPP | GPPE2, GPPE4 | Square End Mills | 1-20 mm; below 55 HRC | Flat floors and shoulders |
| GPP | GPPB2 | Ball Nose End Mills | 1-20 mm; below 55 HRC | Curved surfaces and contours |
| GPP | GPPR4 | Corner Radius End Mills | 1-20 mm; below 55 HRC | Floors with a specified corner radius |
| HPX | HPEX4 | Square End Mills | 3-20 mm; below 55 HRC | Flat floors and shoulders |
| HPX | HPBX2 | Ball Nose End Mills | 1-20 mm; below 55 HRC | Curved surfaces and contours |
| HPX | HPRX4 | Corner Radius End Mills | 3-20 mm; below 55 HRC | Floors with a specified corner radius |
Choose the cutting-data table for the series and operation you are using.
View Steel Cutting ConditionsStarting Conditions by Series and Operation
GP/GPP and HPX have different engagement conditions in these tables. Compare each with your intended cut before selecting a starting value.
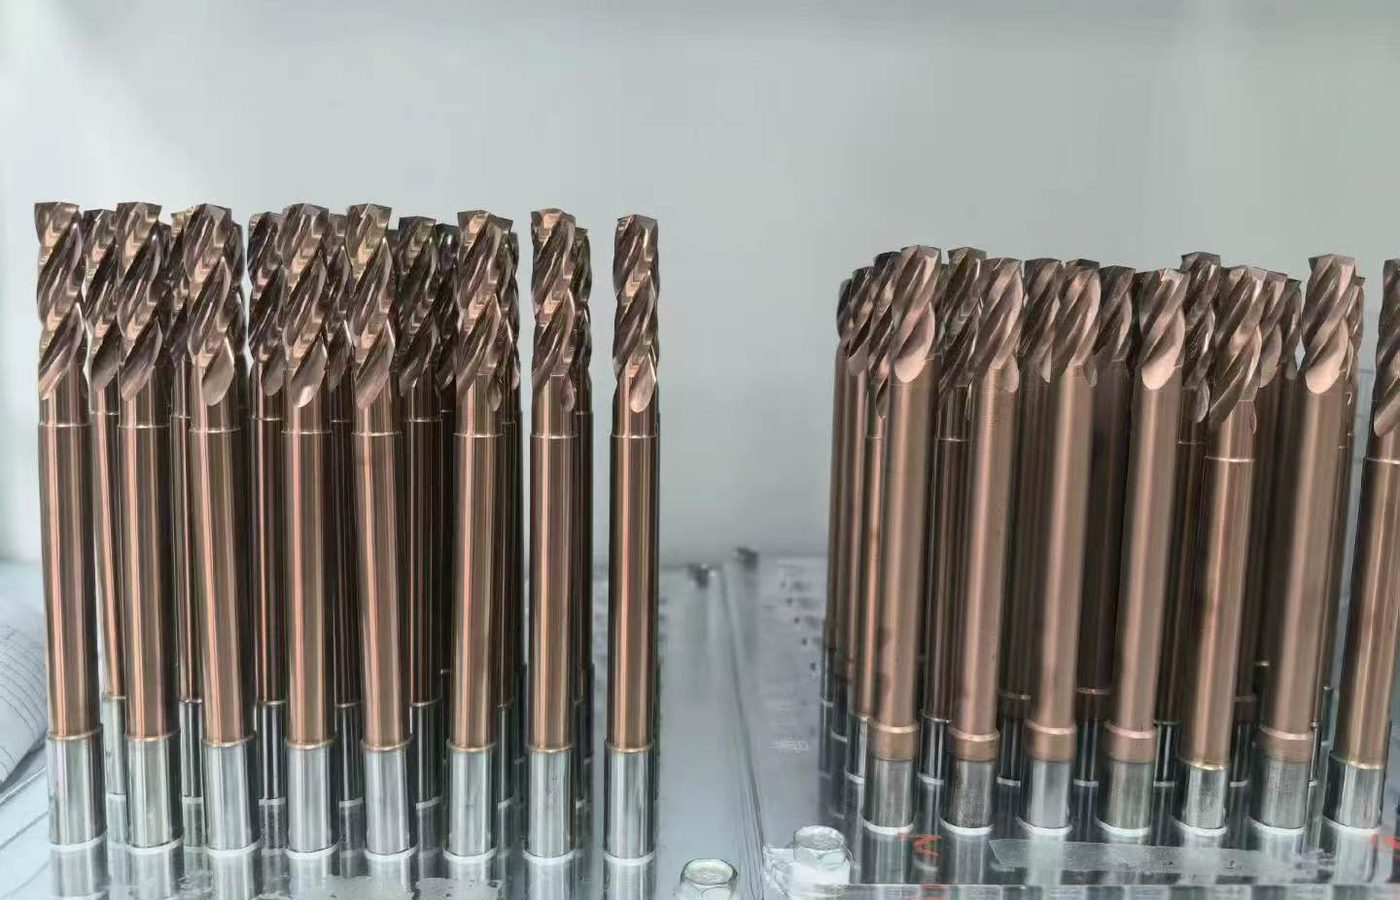
GP and GPP Starting Values
The following GP/GPP values are starting points for profile milling (finishing), Ap = 0.2 D and Ae = 0.3 D. Cutter diameters are 2, 4, 6, 8, 10, 12, 14, 16 and 20 mm. Each fz column gives feed per tooth in mm/tooth for the stated cutter diameter.
| Steel category | Subtype | Condition | HB | Vc (m/min) | fz Ø2 | fz Ø4 | fz Ø6 | fz Ø8 | fz Ø10 | fz Ø12 | fz Ø14 | fz Ø16 | fz Ø20 |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Non-alloy steel | C <= 0.25% | Normalized | 125 | 140-240 | 0.018 | 0.047 | 0.076 | 0.104 | 0.135 | 0.149 | 0.162 | 0.176 | 0.189 |
| Non-alloy steel | 0.25% < C <= 0.55% | Normalized | 190 | 230-330 | 0.020 | 0.052 | 0.084 | 0.116 | 0.150 | 0.165 | 0.180 | 0.195 | 0.210 |
| Non-alloy steel | 0.25% < C <= 0.55% | Quenched and tempered | 210 | 230-330 | 0.020 | 0.052 | 0.084 | 0.116 | 0.150 | 0.165 | 0.180 | 0.195 | 0.210 |
| Non-alloy steel | C > 0.55% | Normalized | 190 | 190-310 | 0.019 | 0.049 | 0.080 | 0.110 | 0.143 | 0.157 | 0.171 | 0.185 | 0.200 |
| Non-alloy steel | C > 0.55% | Quenched and tempered | 300 | 140-240 | 0.018 | 0.047 | 0.076 | 0.104 | 0.135 | 0.149 | 0.162 | 0.176 | 0.189 |
| Non-alloy steel | Free-cutting steel | Quenched and tempered | 220 | 190-310 | 0.019 | 0.049 | 0.080 | 0.110 | 0.143 | 0.157 | 0.171 | 0.185 | 0.200 |
| Low-alloy steel | Not specified | Annealed | 175 | 190-310 | 0.019 | 0.049 | 0.080 | 0.110 | 0.143 | 0.157 | 0.171 | 0.185 | 0.200 |
| Low-alloy steel | Not specified | Normalized | 300 | 140-240 | 0.018 | 0.047 | 0.076 | 0.104 | 0.135 | 0.149 | 0.162 | 0.176 | 0.189 |
| Low-alloy steel | Not specified | Quenched and tempered | 380 | 110-210 | 0.017 | 0.045 | 0.072 | 0.100 | 0.129 | 0.142 | 0.155 | 0.168 | 0.181 |
| Low-alloy steel | Not specified | Quenched and tempered | 430 | 90-190 | 0.016 | 0.043 | 0.069 | 0.095 | 0.123 | 0.135 | 0.148 | 0.160 | 0.172 |
| High-alloy steel / high-alloy tool steel | Not specified | Annealed | 200 | 140-240 | 0.018 | 0.047 | 0.076 | 0.104 | 0.135 | 0.149 | 0.162 | 0.176 | 0.189 |
| High-alloy steel / high-alloy tool steel | Not specified | Quenched and tempered | 300 | 140-240 | 0.018 | 0.047 | 0.076 | 0.104 | 0.135 | 0.149 | 0.162 | 0.176 | 0.189 |
| High-alloy steel / high-alloy tool steel | Not specified | Quenched and tempered | 400 | 110-210 | 0.017 | 0.045 | 0.072 | 0.100 | 0.129 | 0.142 | 0.155 | 0.168 | 0.181 |
HPX Starting Values
The following HPX values are starting points for shoulder milling (finishing), Ap = 1.5 D and Ae = 0.03 D. Cutter diameters are 4, 6, 8, 10, 12, 14, 16, 18 and 20 mm. Each fz column gives feed per tooth in mm/tooth for the stated cutter diameter.
| Steel category | Subtype | Condition | HB | Vc (m/min) | fz Ø4 | fz Ø6 | fz Ø8 | fz Ø10 | fz Ø12 | fz Ø14 | fz Ø16 | fz Ø18 | fz Ø20 |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Non-alloy steel | C <= 0.25% | Normalized | 125 | 160-280 | 0.063 | 0.090 | 0.117 | 0.144 | 0.171 | 0.198 | 0.234 | 0.261 | 0.288 |
| Non-alloy steel | 0.25% < C <= 0.55% | Normalized | 190 | 220-340 | 0.070 | 0.100 | 0.130 | 0.160 | 0.190 | 0.220 | 0.260 | 0.290 | 0.320 |
| Non-alloy steel | 0.25% < C <= 0.55% | Quenched and tempered | 210 | 220-340 | 0.070 | 0.100 | 0.130 | 0.160 | 0.190 | 0.220 | 0.260 | 0.290 | 0.320 |
| Non-alloy steel | C > 0.55% | Normalized | 190 | 200-320 | 0.067 | 0.095 | 0.124 | 0.152 | 0.181 | 0.209 | 0.247 | 0.276 | 0.304 |
| Non-alloy steel | C > 0.55% | Quenched and tempered | 300 | 150-270 | 0.063 | 0.090 | 0.117 | 0.144 | 0.171 | 0.198 | 0.234 | 0.261 | 0.288 |
| Non-alloy steel | Free-cutting steel | Quenched and tempered | 220 | 200-320 | 0.067 | 0.095 | 0.124 | 0.152 | 0.181 | 0.209 | 0.247 | 0.276 | 0.304 |
| Low-alloy steel | Not specified | Annealed | 175 | 200-320 | 0.067 | 0.095 | 0.124 | 0.152 | 0.181 | 0.209 | 0.247 | 0.276 | 0.304 |
| Low-alloy steel | Not specified | Normalized | 300 | 150-270 | 0.063 | 0.090 | 0.117 | 0.144 | 0.171 | 0.198 | 0.234 | 0.261 | 0.288 |
| Low-alloy steel | Not specified | Quenched and tempered | 380 | 120-240 | 0.060 | 0.086 | 0.112 | 0.138 | 0.163 | 0.189 | 0.224 | 0.249 | 0.275 |
| Low-alloy steel | Not specified | Quenched and tempered | 430 | 100-210 | 0.057 | 0.082 | 0.107 | 0.131 | 0.156 | 0.180 | 0.213 | 0.238 | 0.262 |
| High-alloy steel / high-alloy tool steel | Not specified | Annealed | 200 | 150-270 | 0.063 | 0.090 | 0.117 | 0.144 | 0.171 | 0.198 | 0.234 | 0.261 | 0.288 |
| High-alloy steel / high-alloy tool steel | Not specified | Quenched and tempered | 300 | 150-270 | 0.063 | 0.090 | 0.117 | 0.144 | 0.171 | 0.198 | 0.234 | 0.261 | 0.288 |
| High-alloy steel / high-alloy tool steel | Not specified | Quenched and tempered | 400 | 120-240 | 0.060 | 0.086 | 0.112 | 0.138 | 0.163 | 0.189 | 0.224 | 0.249 | 0.275 |
D is cutter diameter; Ap is axial depth and Ae is radial width of cut. Vc is cutting speed in m/min; fz is feed per tooth in mm/tooth. Keep each feed value paired with its stated diameter. These are series-level starting points: the selected end profile and setup still require a trial. See the End Mill Selection Guide, End Mill Coating Guide and End Mill Flute Count Guide for geometry, coating and flute-count considerations.
Changing from profile finishing to a shoulder or slot? Send the intended engagement with your tool reference.
Discuss Steel Cutting ConditionsCheck Tool Support and the Finished Surface
Before a trial, check how the assembled tool reaches the feature and how the machined result will be measured.
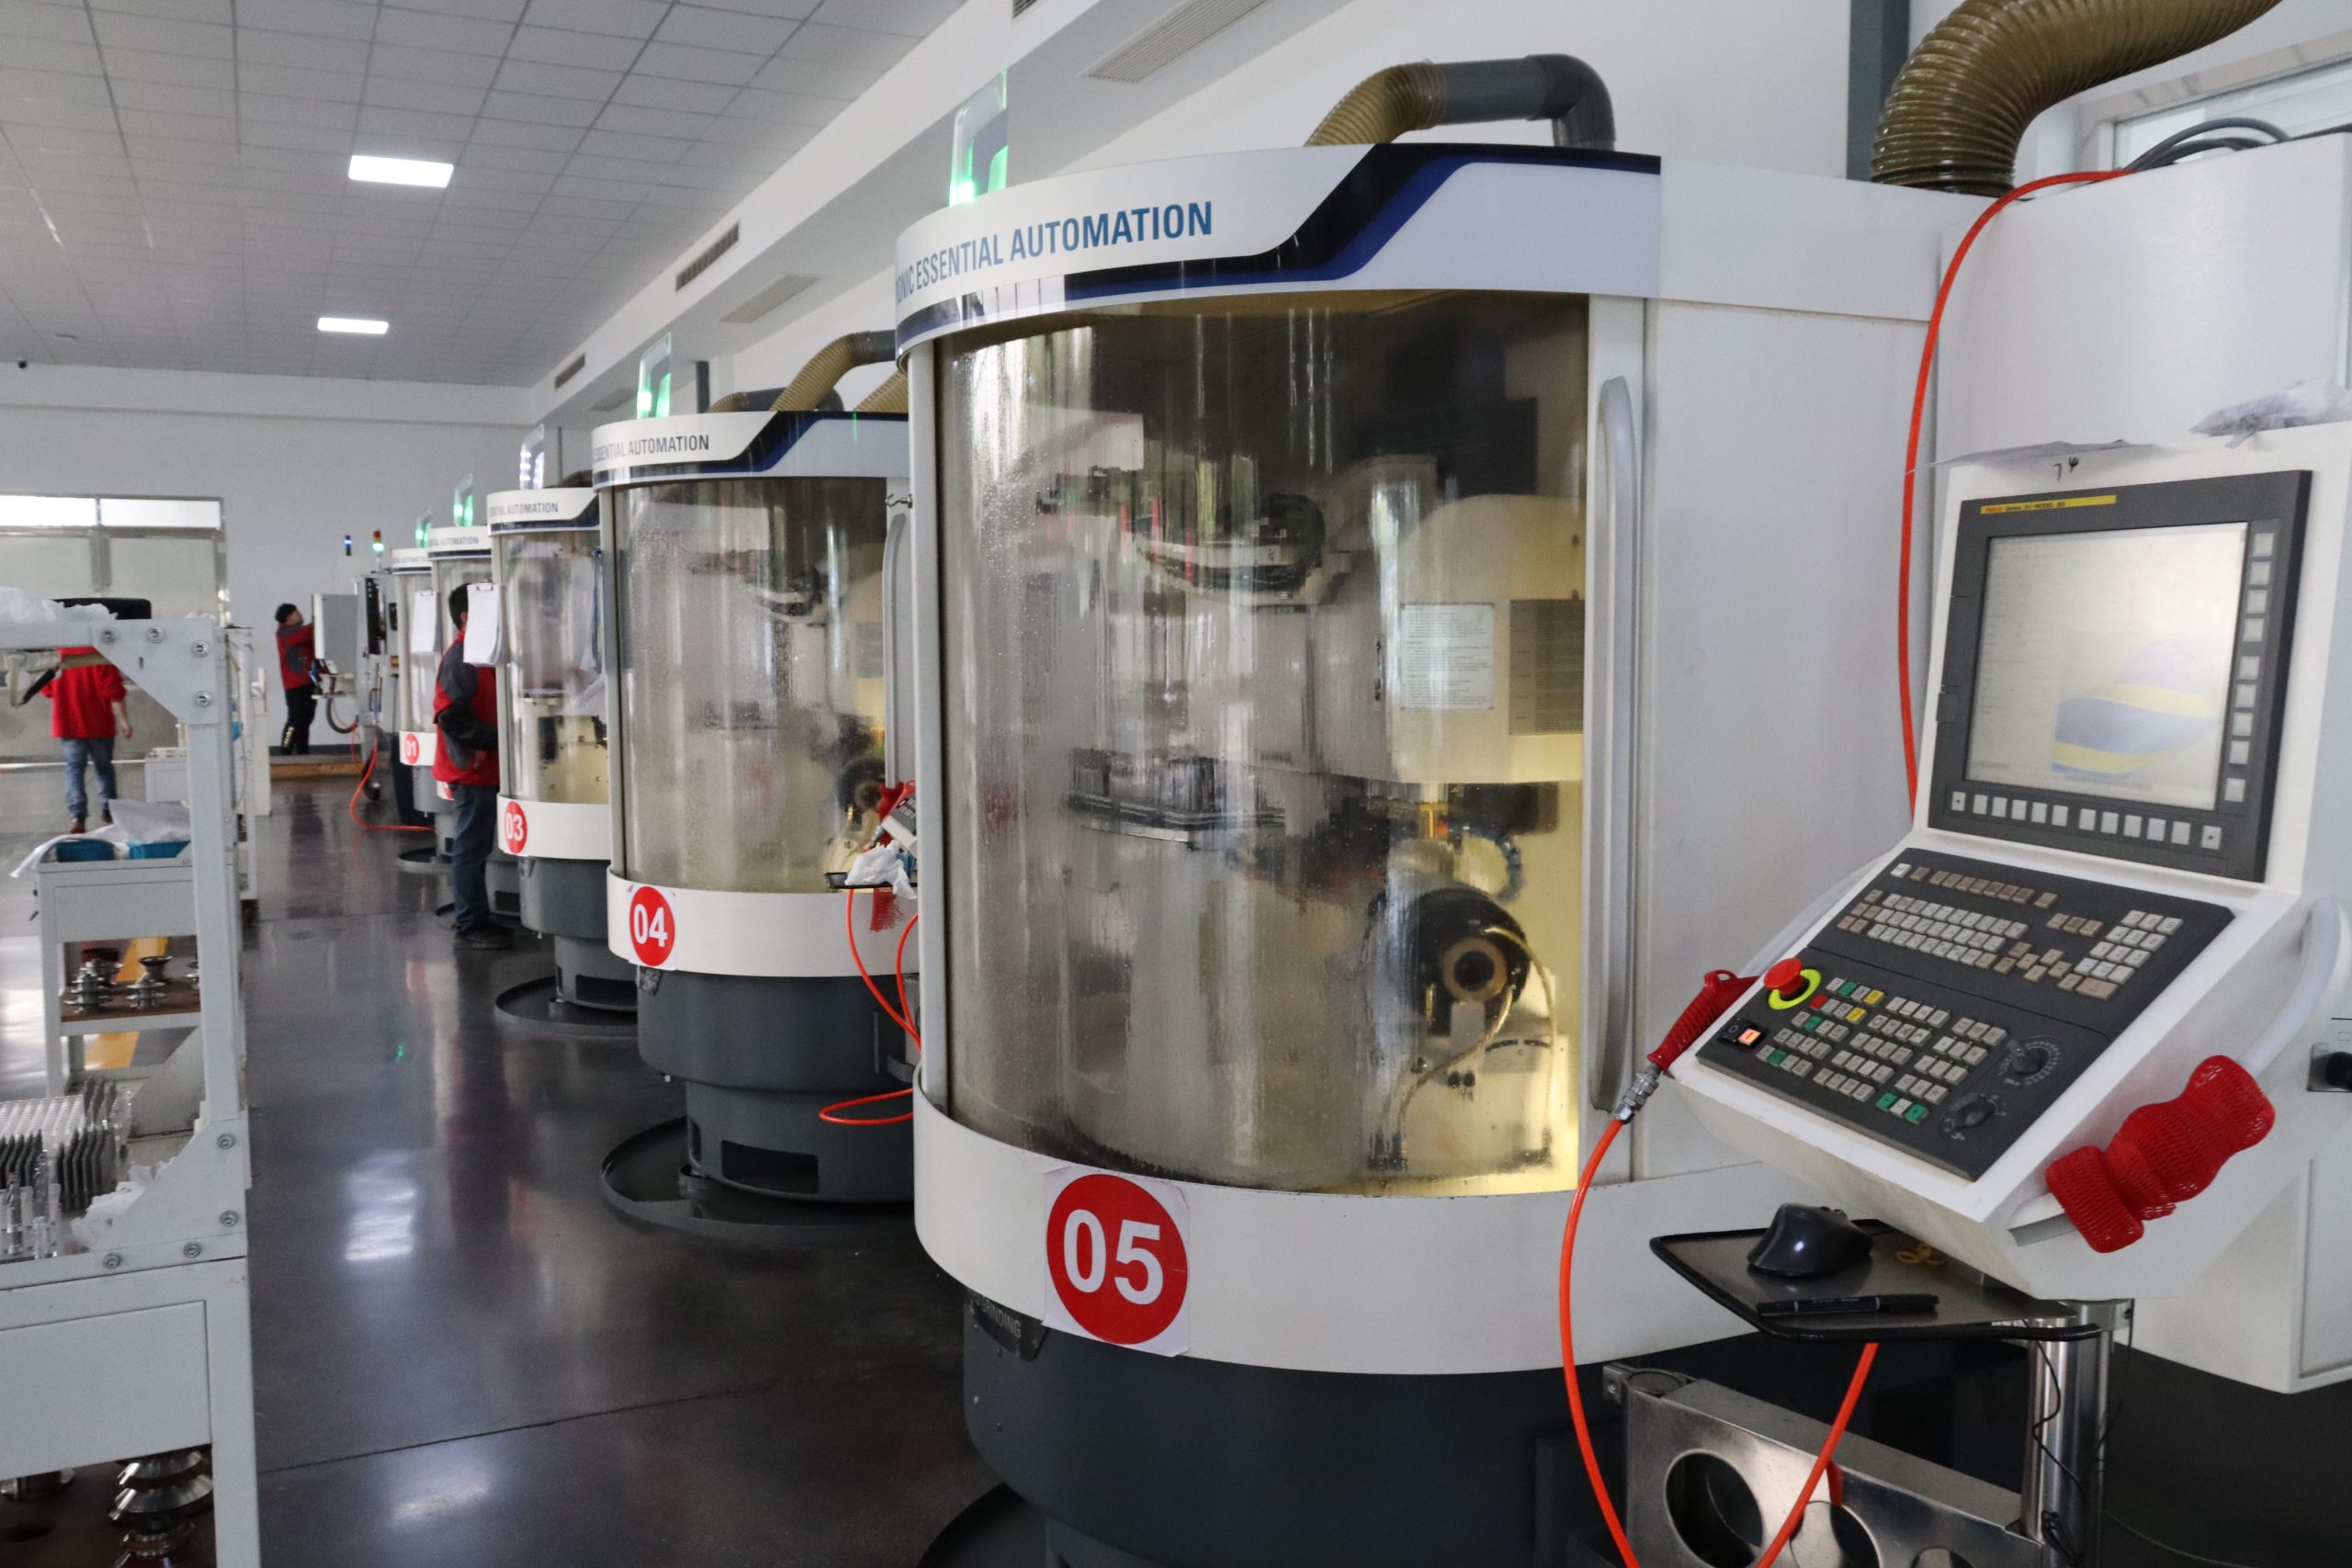
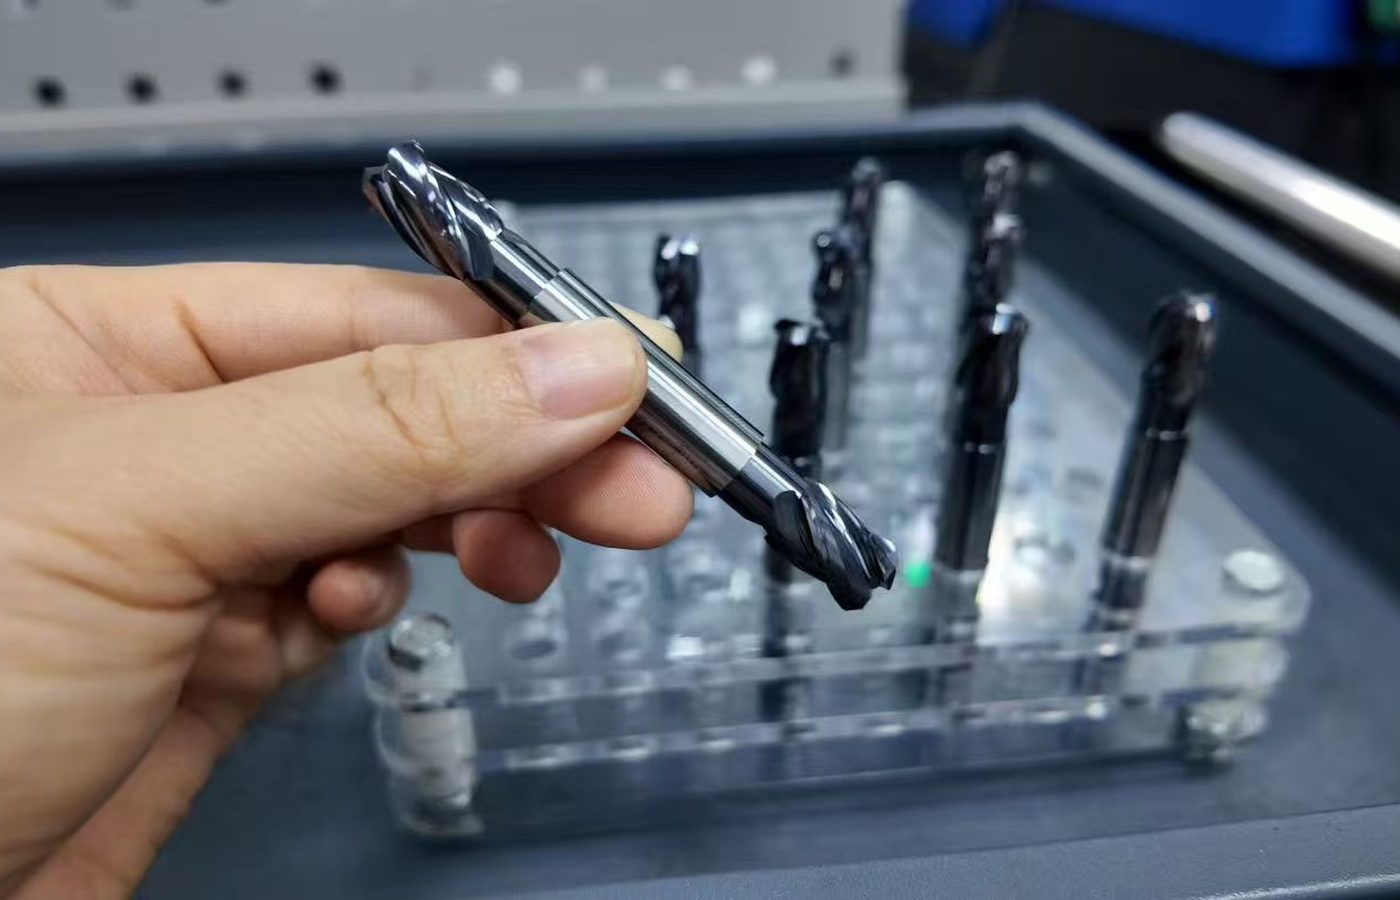
Support and clearance
Use the shortest projection that reaches the feature. Check the holder and tool body through the complete machining path, including entry and exit.
Tool and part measurements
Identify the cutting dimensions that need inspection separately from the part tolerance and surface finish. Tool-measurement equipment is described in Factory and Quality Control; use Downloads for dimensional drawings.
Use the model drawing to check the full dimensions before ordering.
Find Tool DrawingsOrder a Standard Tool or Discuss a Drawing
Choose a standard model when its profile and working dimensions fit the part. For an unavailable size or clearance, a drawing defines what needs to change.
Standard sizes
Use the selected end profile and full dimensions to identify the tool. Include the model code and quantity when requesting a repeat order.
A tool to your drawing
If the required diameter, reach or profile is unavailable, email a dimensioned drawing for Custom Cutting Tools. Mark the critical geometry and tolerances, with the steel grade and hardness.
MOQ is normally 5–10 pieces, confirmed by quotation. Samples and sample freight are charged. Production timing is confirmed for the order; shipping time is stated separately. See Ordering and Delivery for purchasing terms.
Email the drawing with the material and critical dimensions to discuss the tool you need.
Discuss a Custom ToolSteel Milling Questions
Can I select an end mill from steel hardness alone?
No. Hardness narrows the options, but the steel grade, heat-treatment condition, end profile and machining operation must also match the tool.
Are the GP/GPP and HPX tables directly comparable?
They describe different cuts. GP/GPP values are for profile finishing at Ap = 0.2 D and Ae = 0.3 D; HPX values are for shoulder finishing at Ap = 1.5 D and Ae = 0.03 D. Compare tools under the same actual operation.
Does a ball nose leave the same floor as a square end mill?
No. A square end mill has a flat cutting end. A ball nose has a rounded profile for curved surfaces; choose it to suit the part contour and toolpath.
What if I need more reach than the standard tool provides?
Compare the cutting length, body clearance and projection after clamping. If the available dimensions cannot reach the feature, email a section drawing with the required depth and clearance.