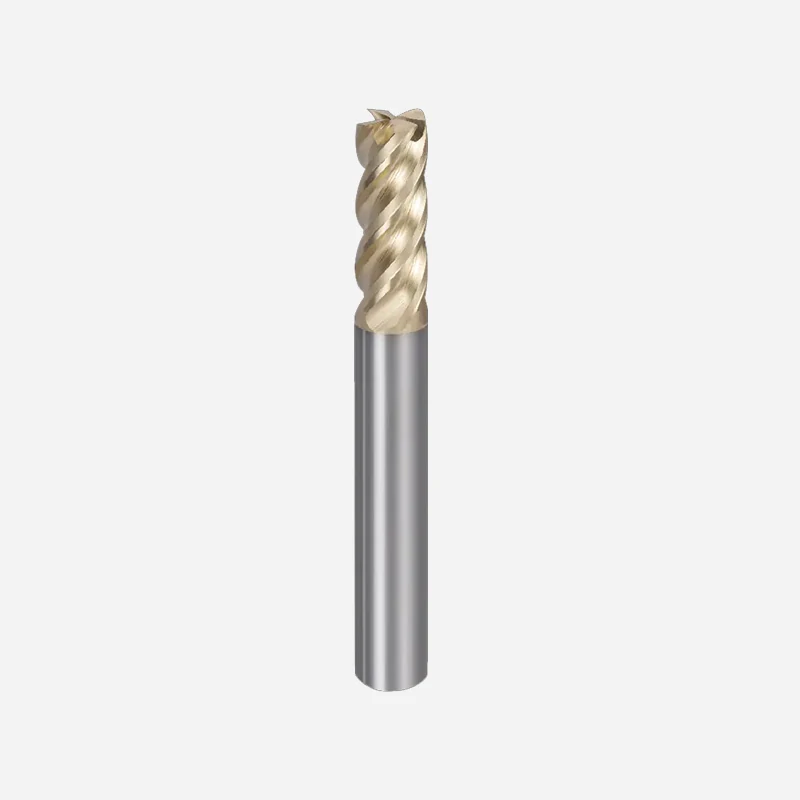
MSME4
Square End Mills
- End profile
- Square End Mills
- Cutting diameter
- 1-20 mm
- Coating and geometry
- ZrN; unequal helix
- Part feature
- Flat floors and shoulders; check any corner treatment on the selected model.

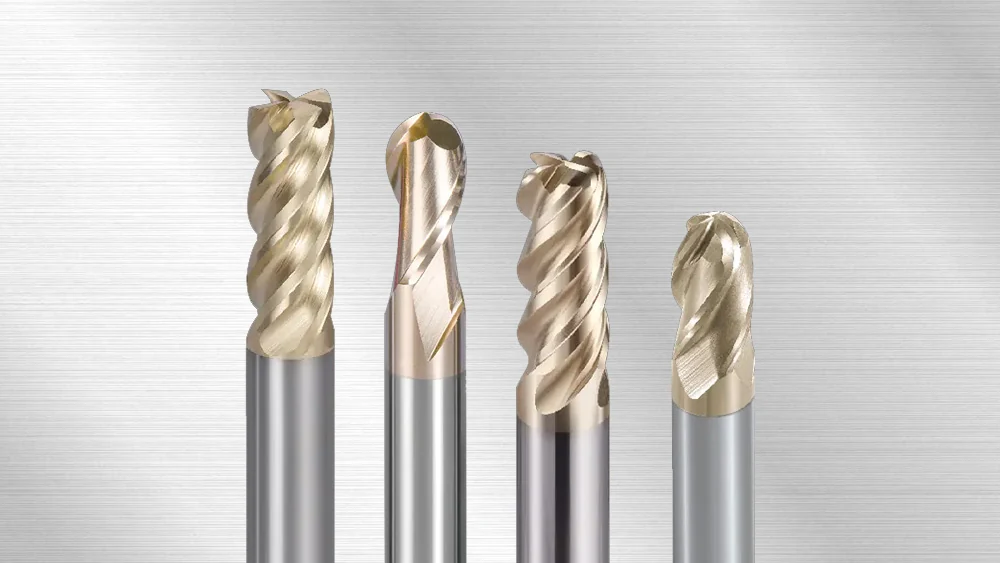
Choose an end mill for titanium around the alloy condition and the feature you need to machine. MSME4 square-end and MSMR4 corner-radius tools provide two cutting profiles for flat floors, shoulders and radiused corners.
Pure titanium, age-hardened alpha + beta alloy and beta alloy have separate starting-data entries below. Match the actual grade and condition before choosing cutting conditions; a broad alloy category does not identify a specific commercial grade.
Send the titanium grade and part detail, or a tool code and quantity for a repeat order.
Find a Titanium Milling ToolUse the material designation, condition and available hardness or tensile data to identify the workpiece. Then choose the cutting profile and reach around the part.
When a process already exists, use its tool wear, chips and finished surface as comparison points. Keep the tool reference and cutting conditions with those observations.
Compare the cutting profiles and dimensions needed for your part.
Compare Titanium Milling ToolsMSME4 and MSMR4 are four-flute tools with ZrN coating and an unequal helix. Select the end profile first, then the size and working length.
MSME4
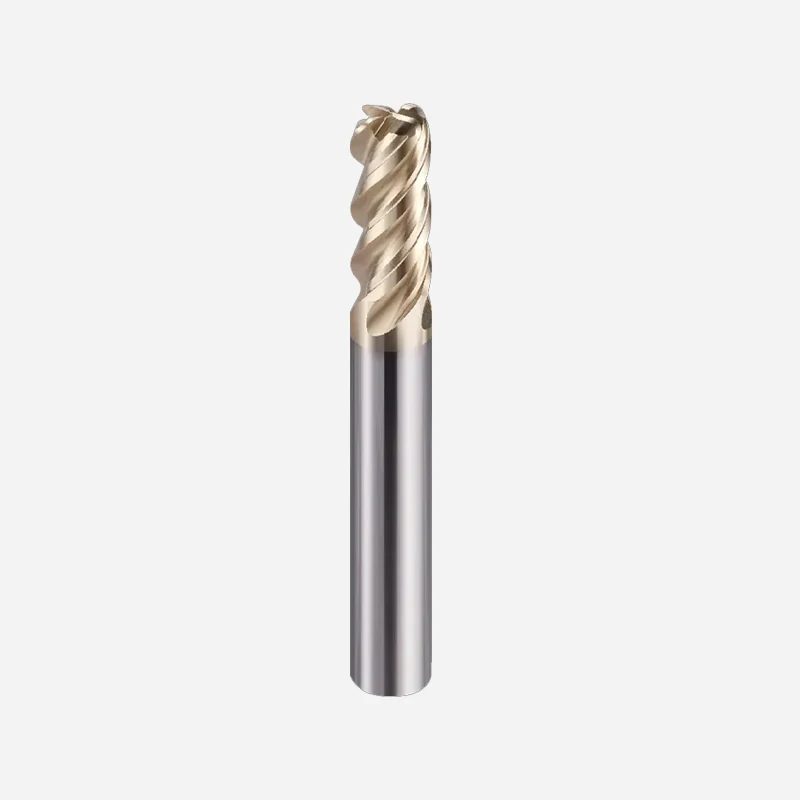
MSMR4
Other cutting profiles
Carbide End Mills includes other end profiles for features that a flat or corner-radius tool cannot produce.
Changing the workpiece material
For stainless workpieces, use Stainless Steel Milling. A shared tool family does not make the titanium and stainless starting conditions interchangeable.
Check the material row and engagement before using a starting value.
View Starting Cutting ConditionsThe following MSM values are starting points for shoulder milling (finishing), Ap = 1.5 D and Ae = 0.03 D. Cutter diameters are 2, 4, 6, 8, 10, 12, 16 and 20 mm. Each fz column gives feed per tooth in mm/tooth for the stated cutter diameter.
| Titanium category | Subtype / condition | HB | Tensile strength (N/mm²) | Vc (m/min) | fz Ø2 | fz Ø4 | fz Ø6 | fz Ø8 | fz Ø10 | fz Ø12 | fz Ø16 | fz Ø20 |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Titanium alloy | Pure titanium | 200 | 680 | 70-100 | 0.046 | 0.074 | 0.101 | 0.132 | 0.156 | 0.182 | 0.231 | 0.277 |
| Titanium alloy | Alpha + beta alloy, age-hardened | 375 | 1260 | 70-100 | 0.046 | 0.074 | 0.101 | 0.132 | 0.156 | 0.182 | 0.231 | 0.277 |
| Titanium alloy | Beta alloy | 410 | 1400 | 30-55 | 0.032 | 0.050 | 0.069 | 0.090 | 0.107 | 0.124 | 0.158 | 0.189 |
D is cutter diameter, Ap axial depth and Ae radial width of cut. Vc is cutting speed; fz is feed per tooth. Use the fz column for the selected cutter diameter. These MSM series-level values describe the stated shoulder-finishing cut, not a universal titanium setting.
For Ti-6Al-4V or another named grade, match its condition and material properties to the relevant row before a trial. Keep the selected tool, engagement, projection and coolant delivery consistent when comparing results. The End Mill Selection Guide, End Mill Coating Guide and End Mill Flute Count Guide explain the related choices.
Need help with wear or finish? Email the tool edge and part photos with the current cutting conditions.
Discuss a Titanium Milling ProblemA tool can have the right end profile and still need a different length or mounting arrangement to reach the feature.
Check the body and holder against the entry path and adjacent walls. Use the shortest projection that reaches the feature.
Check coolant delivery at the cutting zone and the path for chips to leave. Compare tool wear and the finished surface under the actual cutting conditions.
Use Downloads for the model drawing and specify any required dimensional report. Factory and Quality Control provide equipment and measurement information.
Use the model drawing to check the full dimensions before ordering.
Find Tool DrawingsChoose a standard model when its profile and working dimensions fit the part. For an unavailable size or clearance, a drawing defines what needs to change.
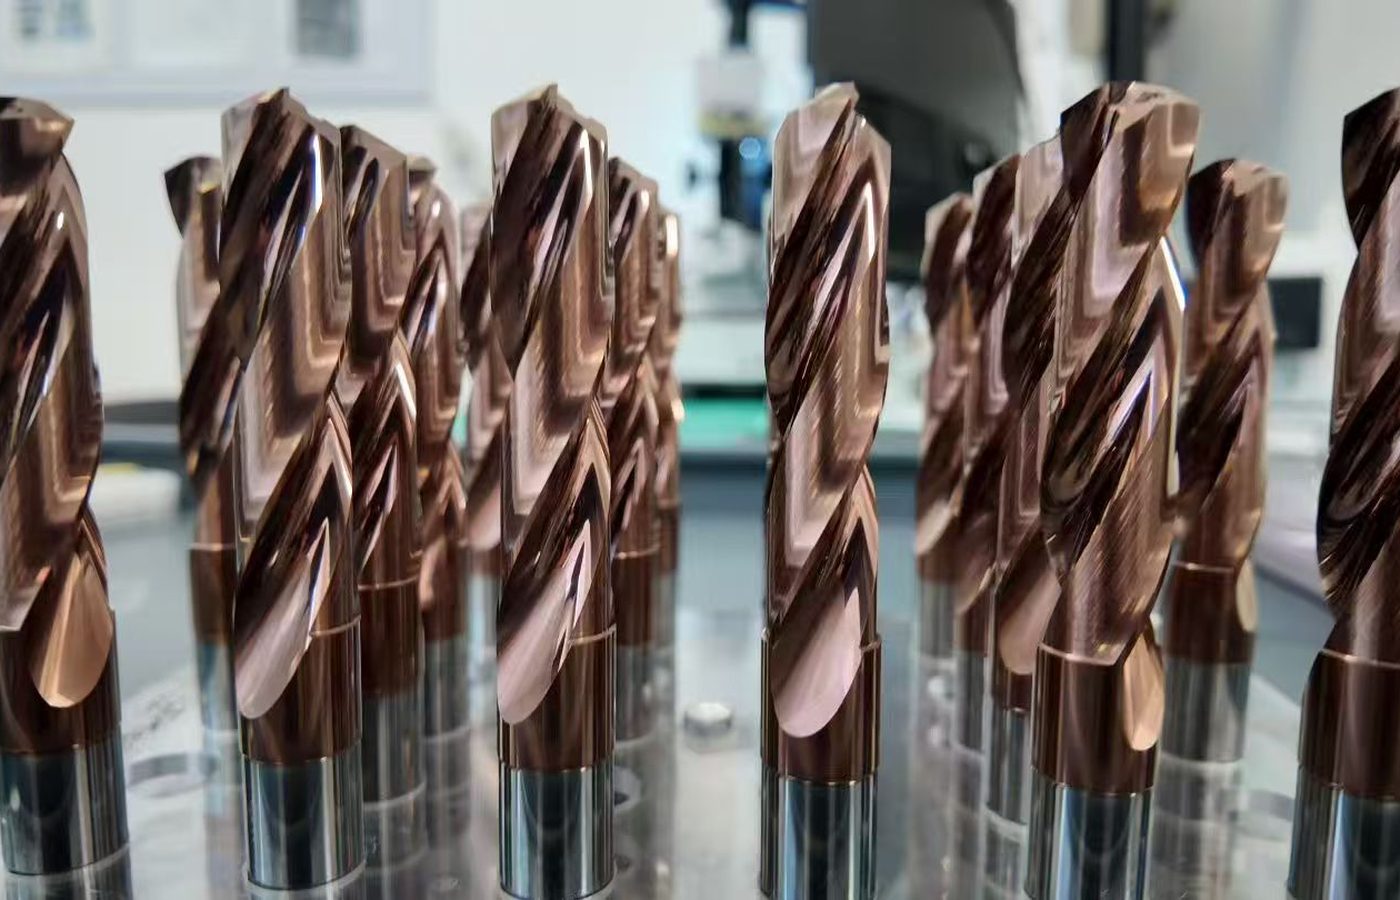
MOQ is normally 5–10 pieces, confirmed by quotation. Samples and sample freight are charged. Production timing is confirmed for the order; shipping time is stated separately. See Ordering and Delivery for purchasing terms.
Email the drawing with the material and critical dimensions to discuss the tool you need.
Discuss a Custom ToolStart with the alloy designation and condition, then match the end profile, diameter and cutting length to the part. Check mounted reach and select cutting conditions for that tool and operation.
Not from the category name alone. The row states an age-hardened condition and material-property references. Compare the actual Ti-6Al-4V condition with those details before selecting a starting point.
The table describes shoulder finishing at Ap = 1.5 D and Ae = 0.03 D. A full slot changes the engagement and requires separate cutting conditions.
No. Cutting length is the available cutting edge. Reach also depends on the body geometry, clamped length and holder clearance. Check all three against the feature.